"Adding Value to Life in Beauty and Skin Care Science"
From molecular research and botanical extract stabilization to classified cleanroom compounding and automated packaging, our work represents modern cosmetic manufacturing excellence in Nepal.
 Research & Development 100% Tested Actives
Formulating skin-identical lipid matrices, photostable UV shields, and targeted actives tailored for South Asian skin and varied environmental climates.
 Cleanroom Production Classified Cleanroom Suites
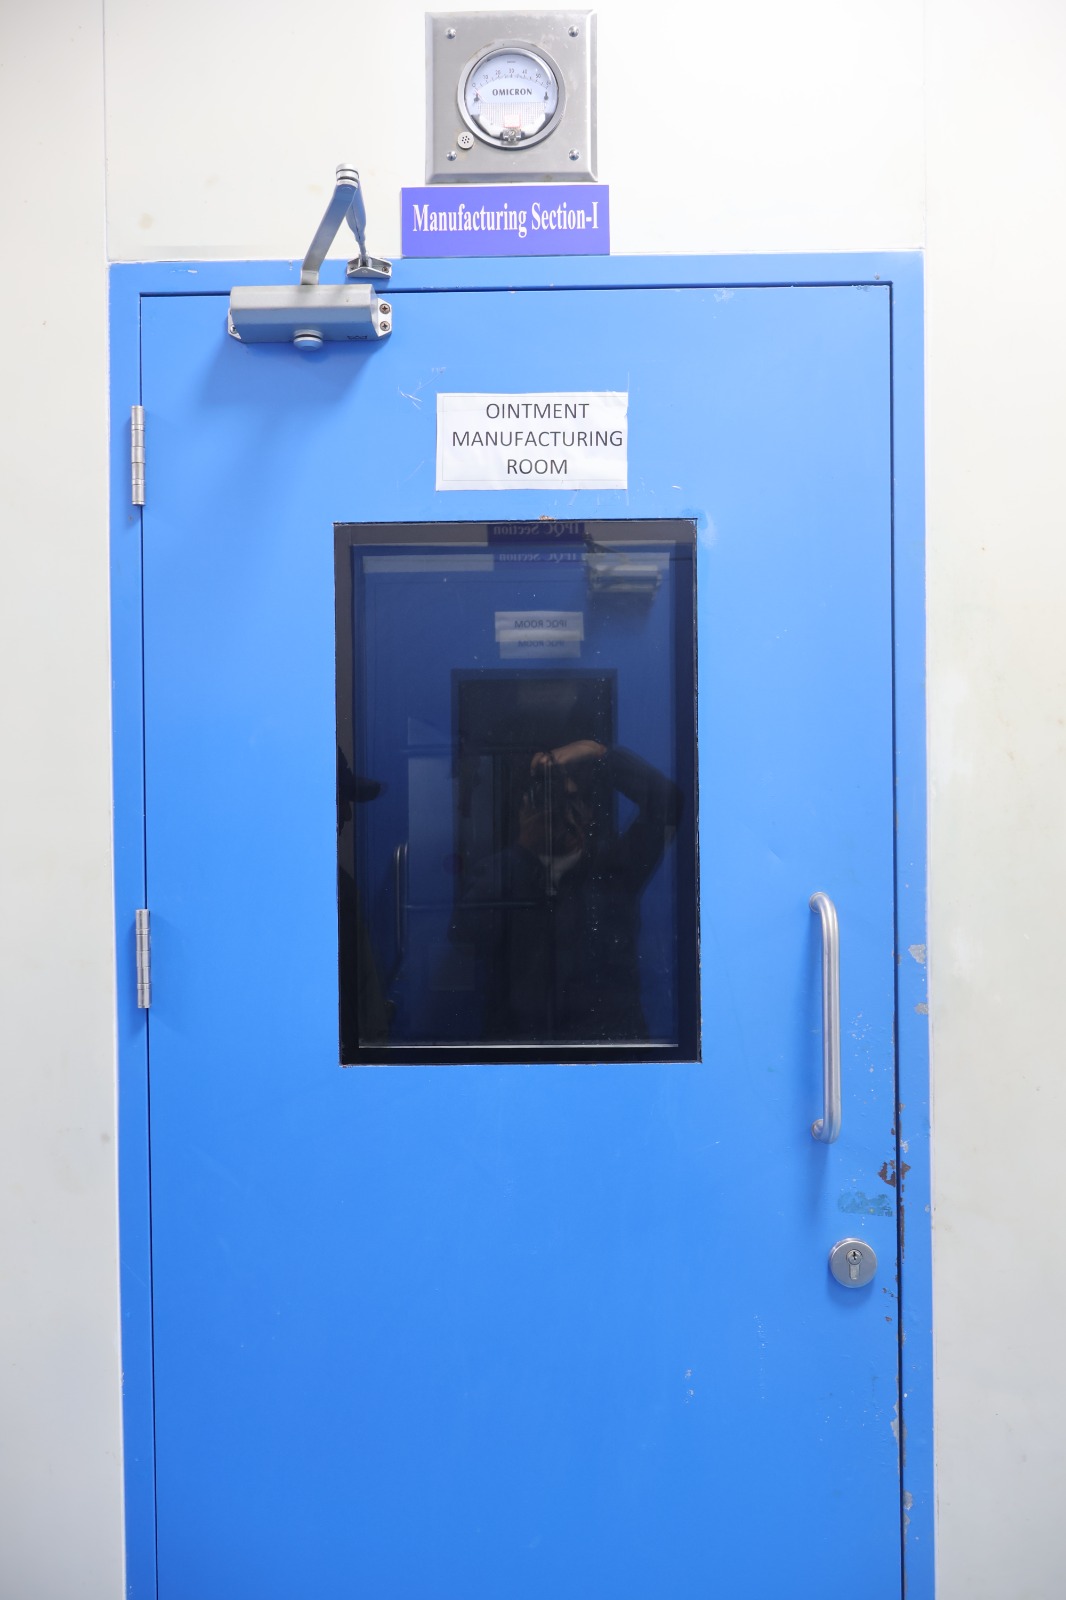
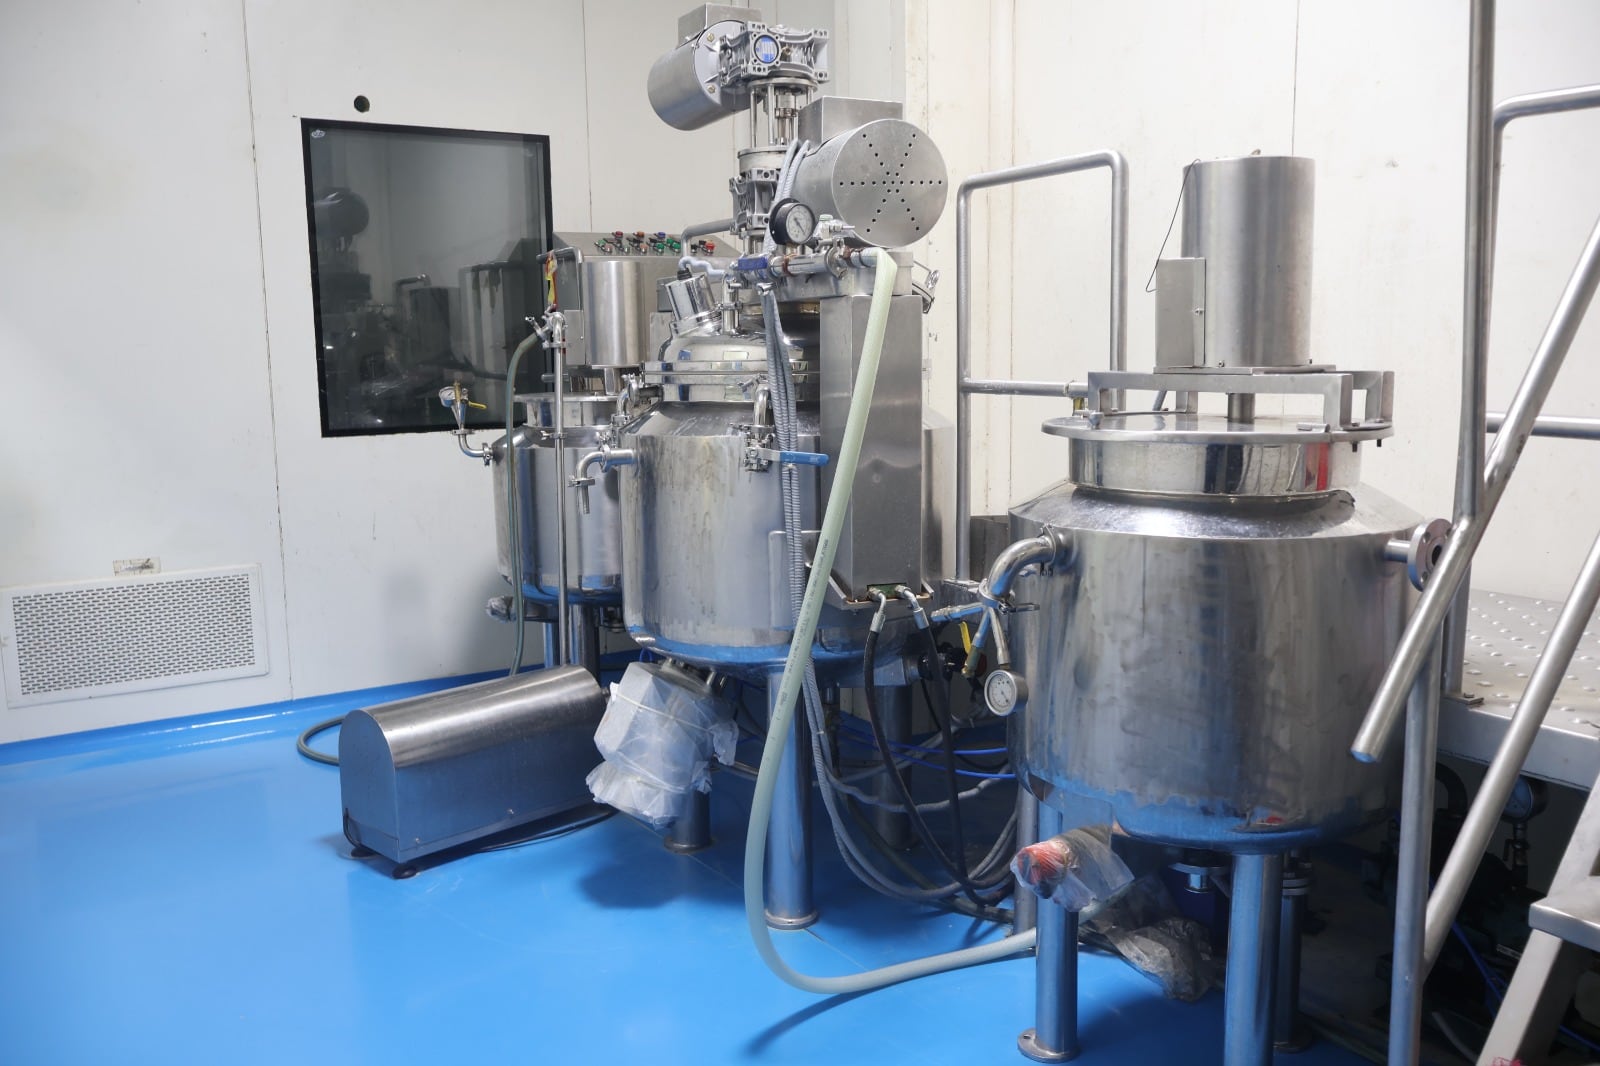
Operating negative-pressure cleanroom suites with sanitary stainless steel homogenizers preventing microbial and particulate contamination.
 Automation Machinery High-Volume Automation
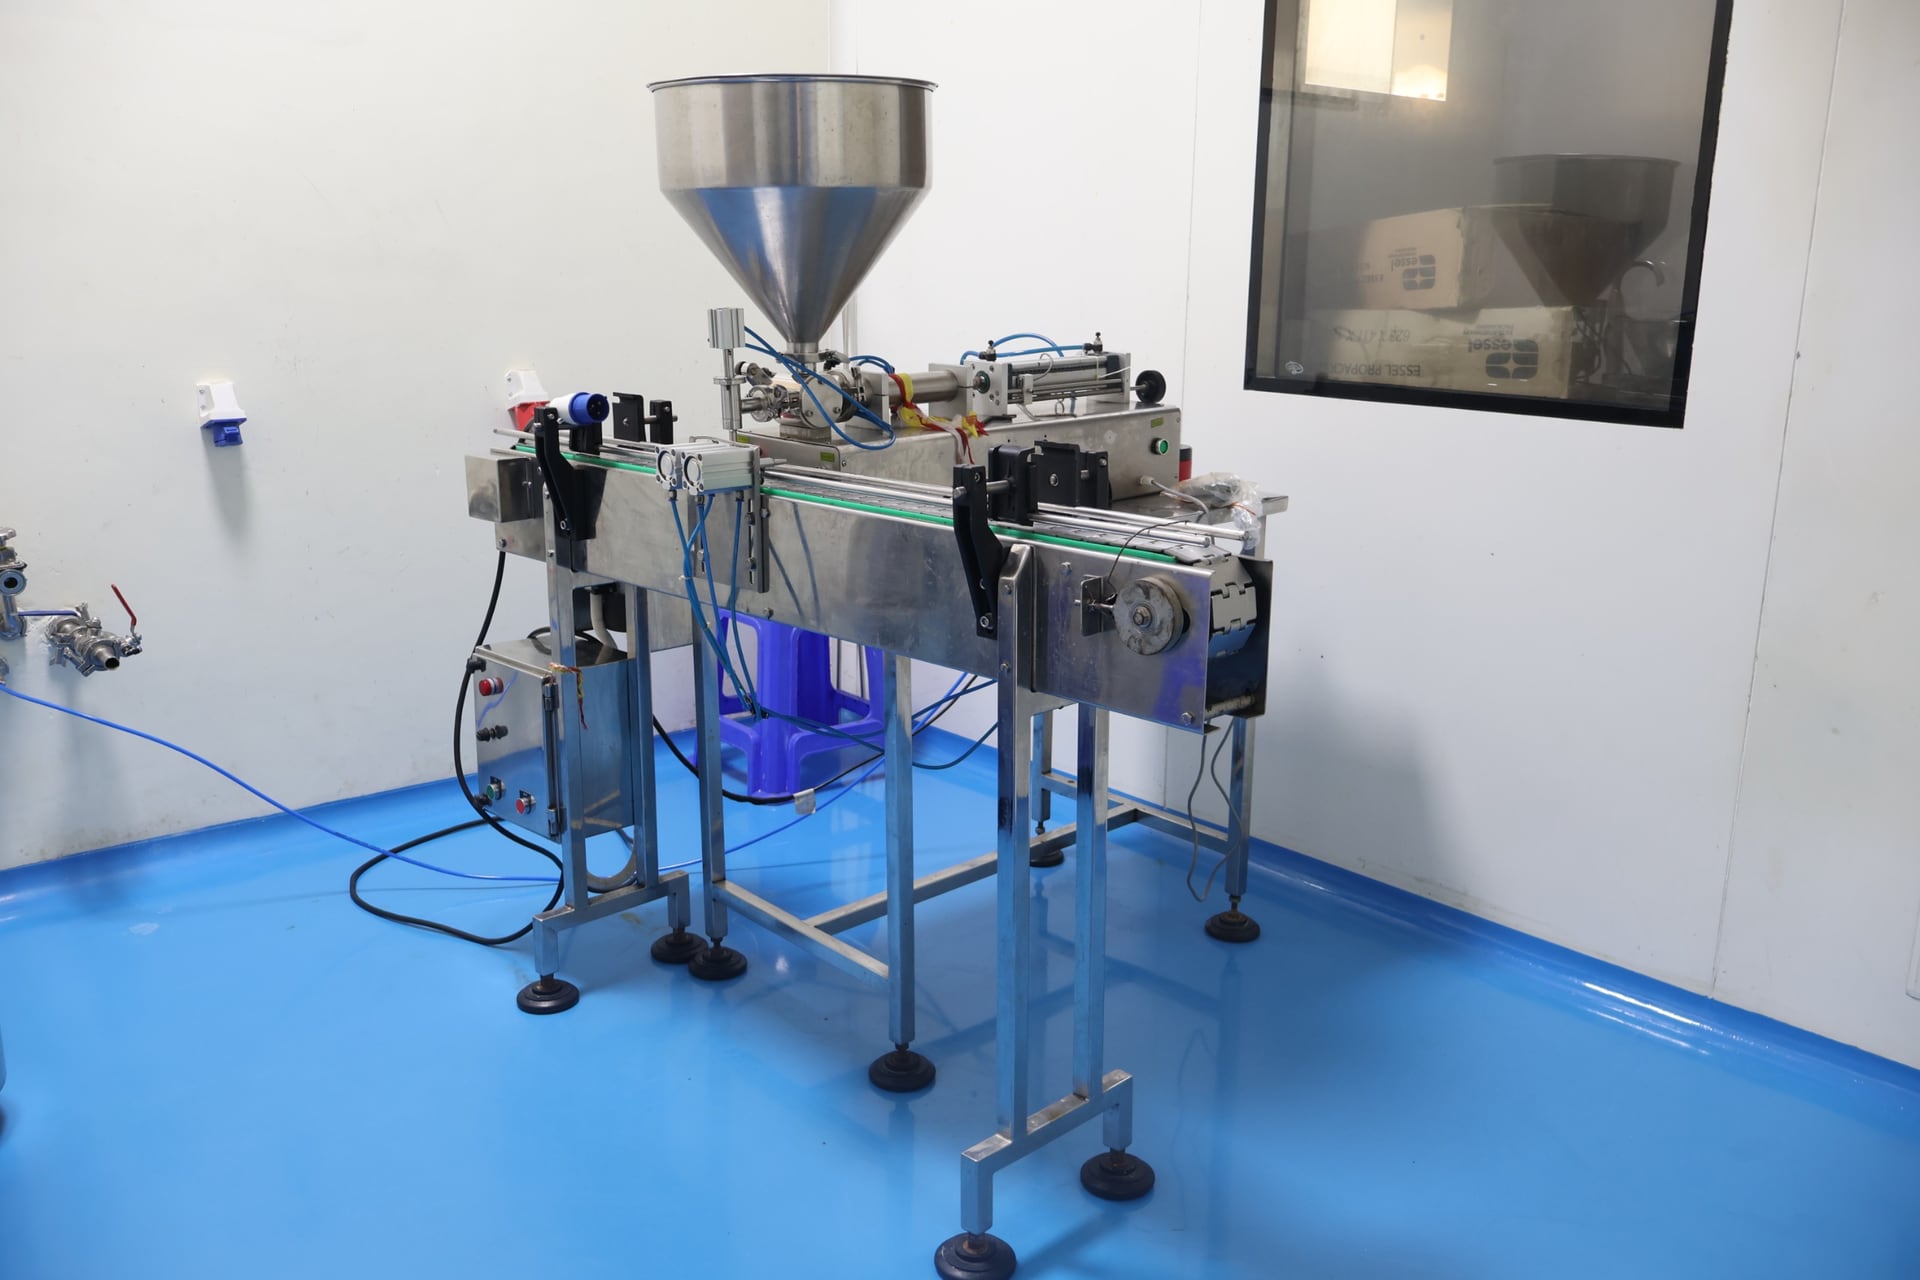
Automated volumetric piston filling, ultrasonic tube crimping, and precision liquid bottling lines meeting high nationwide distribution volume.
 Quality Control Strict Batch Release Protocol
Every single production batch undergoes stringent in-house physico-chemical and bio-burden assay verification before commercial dispatch.
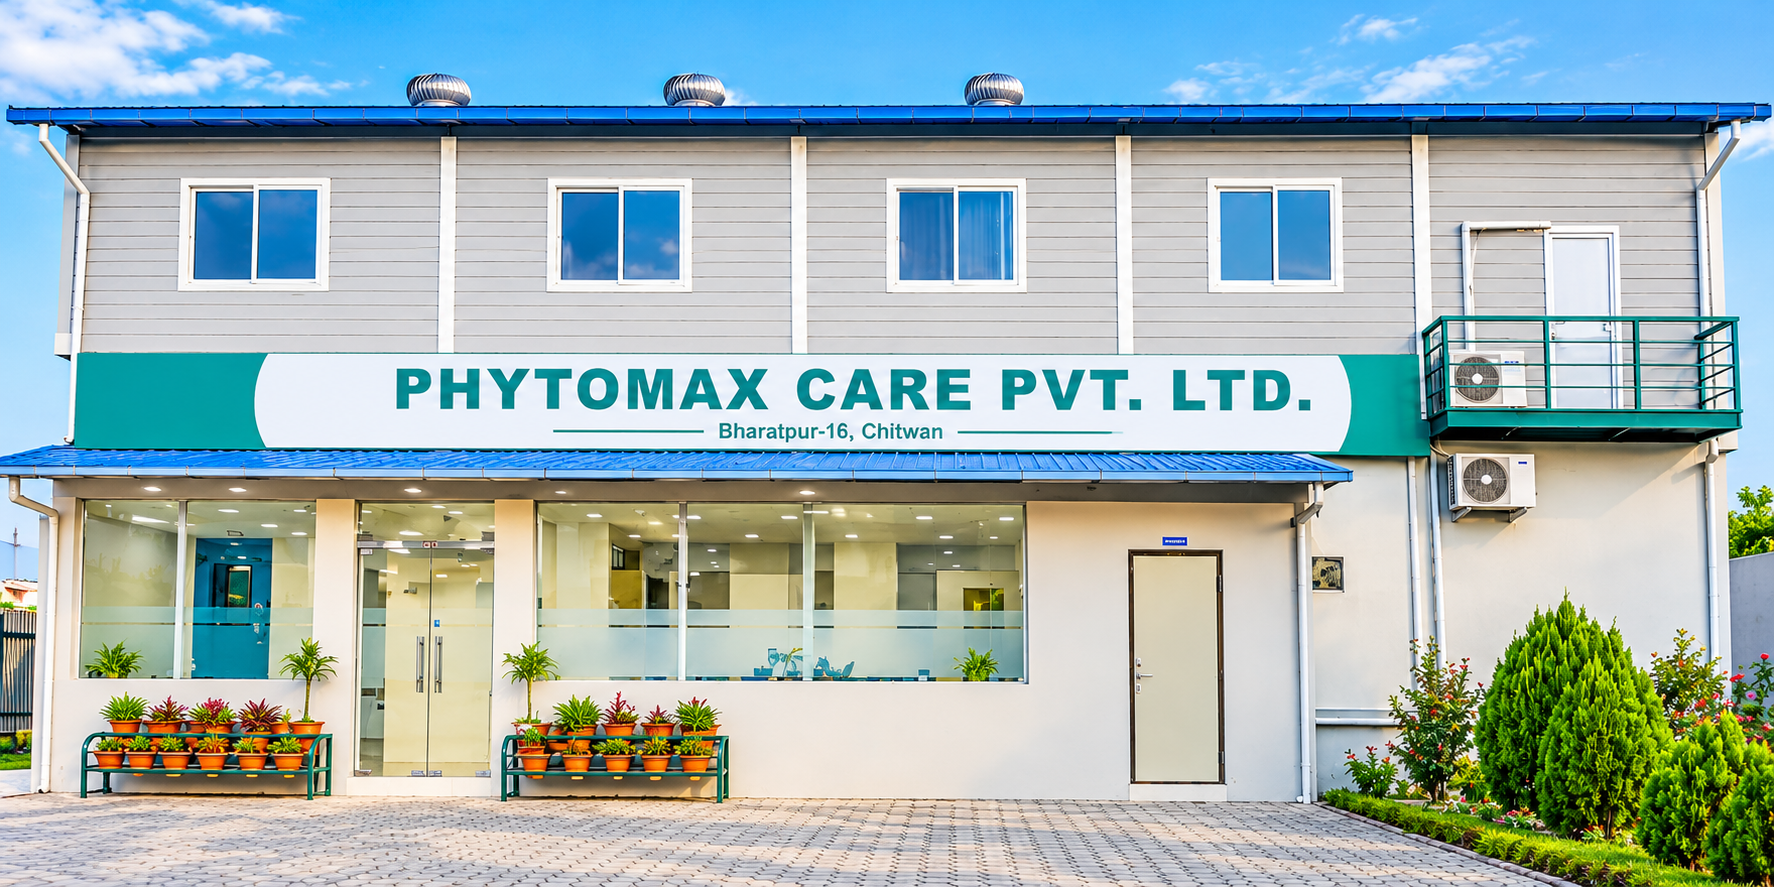
Phytomax Care operates a specialized, controlled-atmosphere production facility in Bharatpur-16, Chitwan, Nepal equipped with negative-pressure cleanroom suites, automated compounding and packaging machinery, and dedicated analytical research laboratories.
 Facility Architecture
Modern manufacturing and administrative headquarters with secure materials entry and dedicated logistics access.
Cleanroom Production Classified cleanroom environment featuring stainless steel sanitary blending tanks with jacketed heating and vacuum homogenization.
Manufacturing Plant Pharmaceutical-grade cosmetic compounding and bulk manufacturing plant equipped with jacketed stainless-steel reactors, high-shear homogenizers, and sanitary piping.
Automated Packaging High-precision volumetric automated jar filling line ensuring sterile dosing, hermetic closure, and contamination-free barrier cream packing.
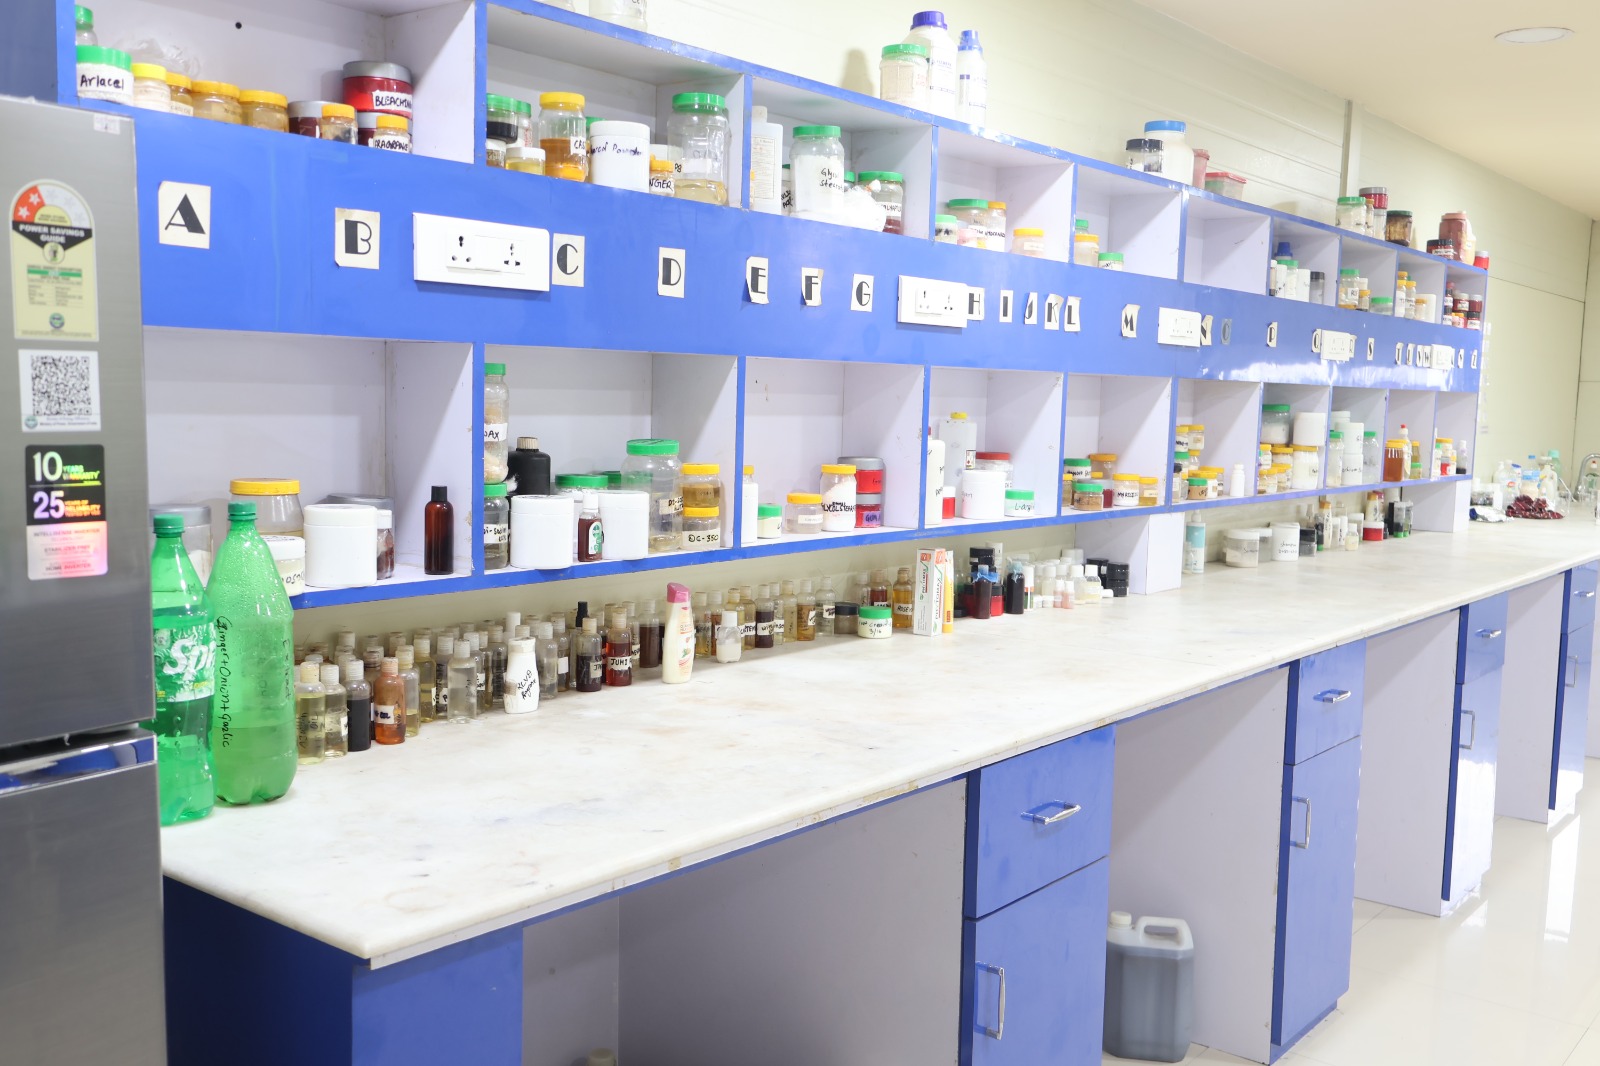
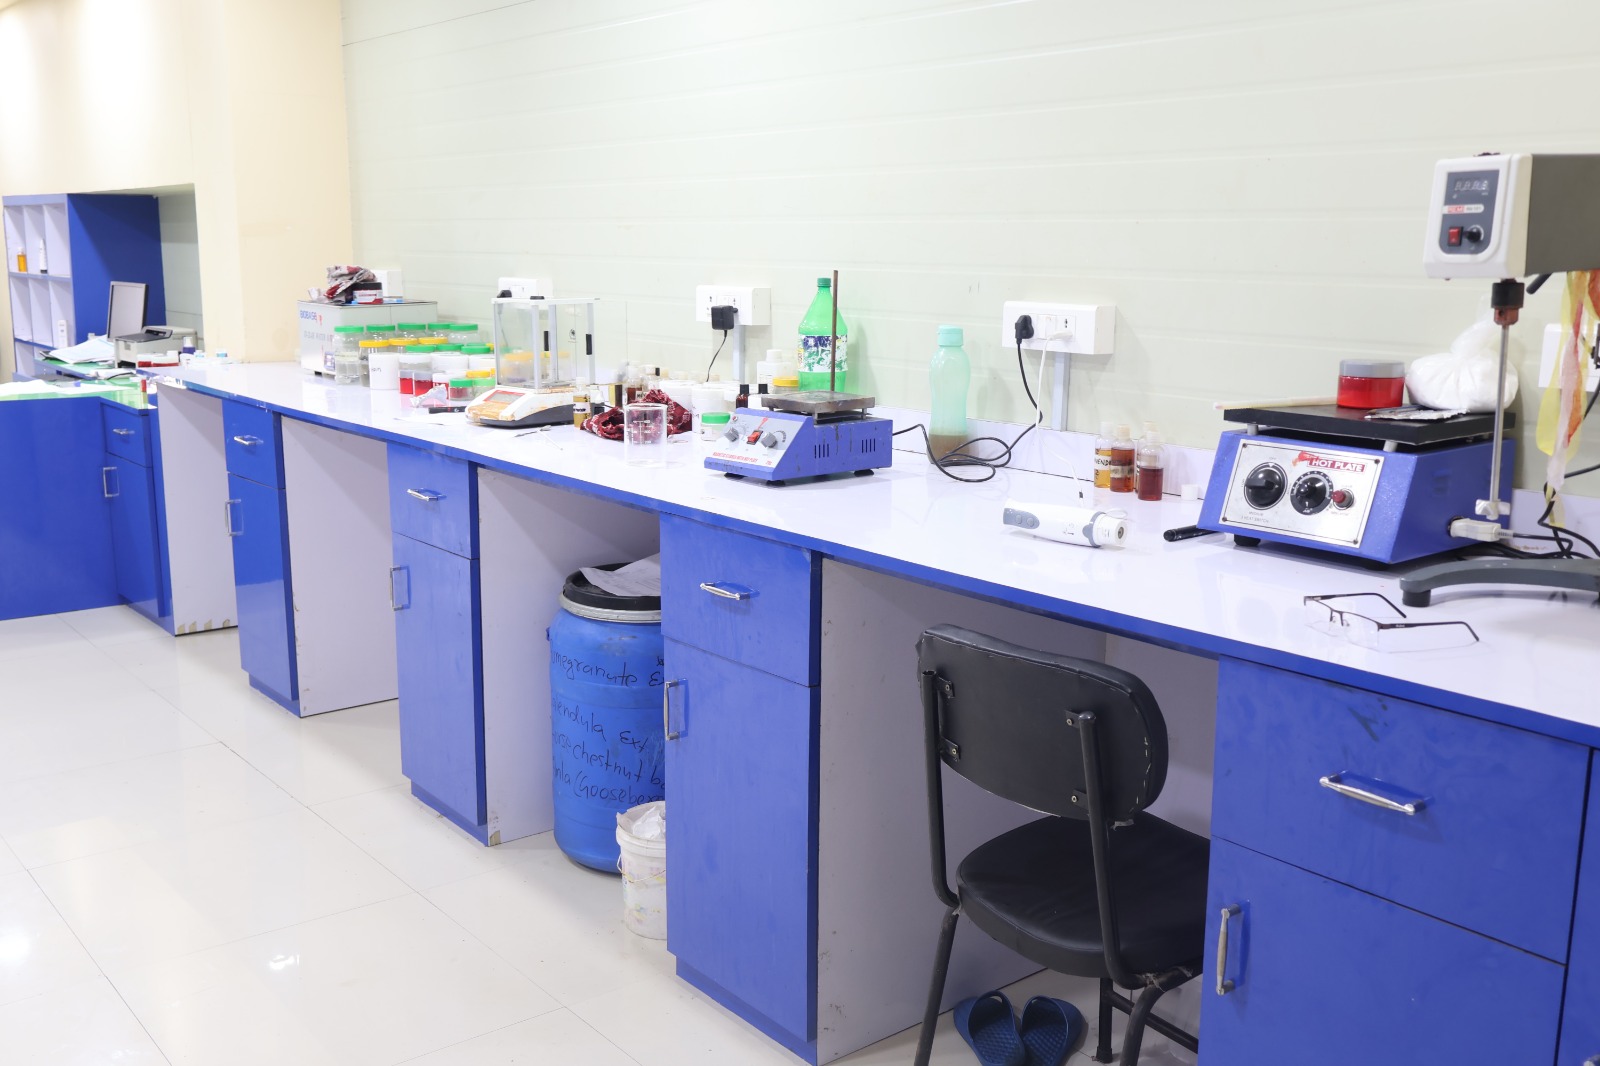
Research & Development Dedicated laboratory for viscosity testing, refractive index verification, emulsion stability analysis, and pH calibration.
Quality Control Precision spectrophotometric and bio-burden testing benches ensuring strict microbiological compliance before release.
 Cleanroom Infrastructure
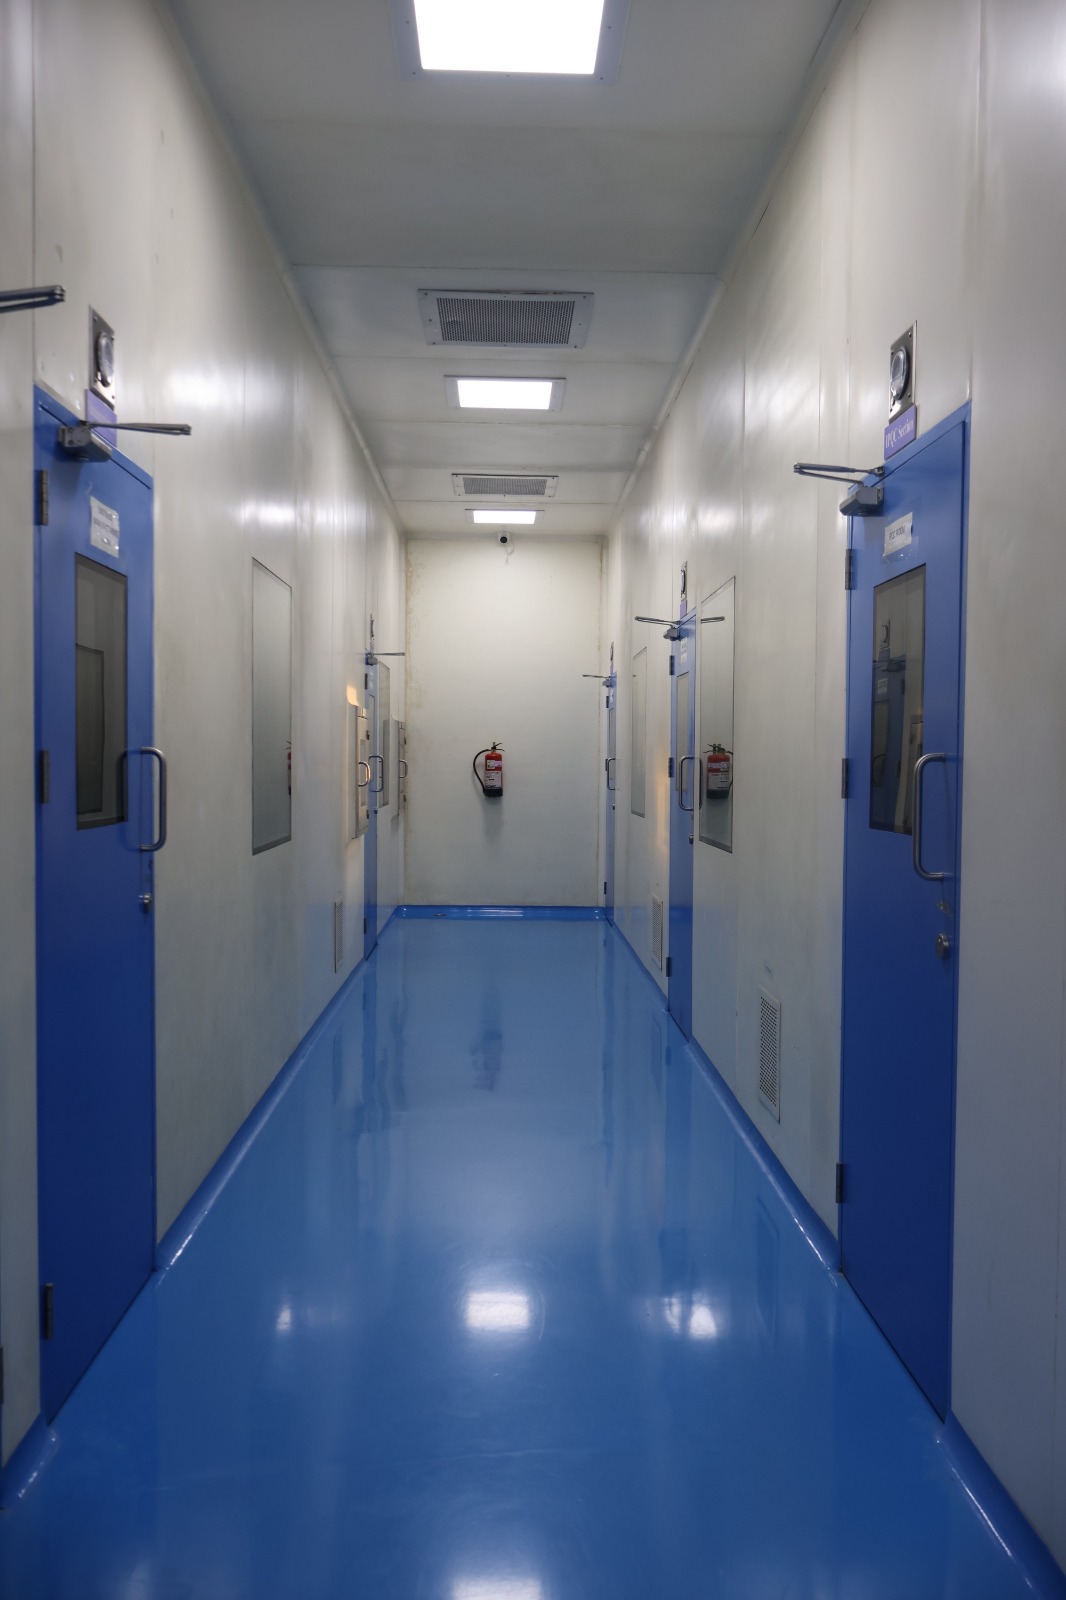
Anti-static, sealed cleanroom corridors with interlocking differential pressure airlocks between gowning and production zones.
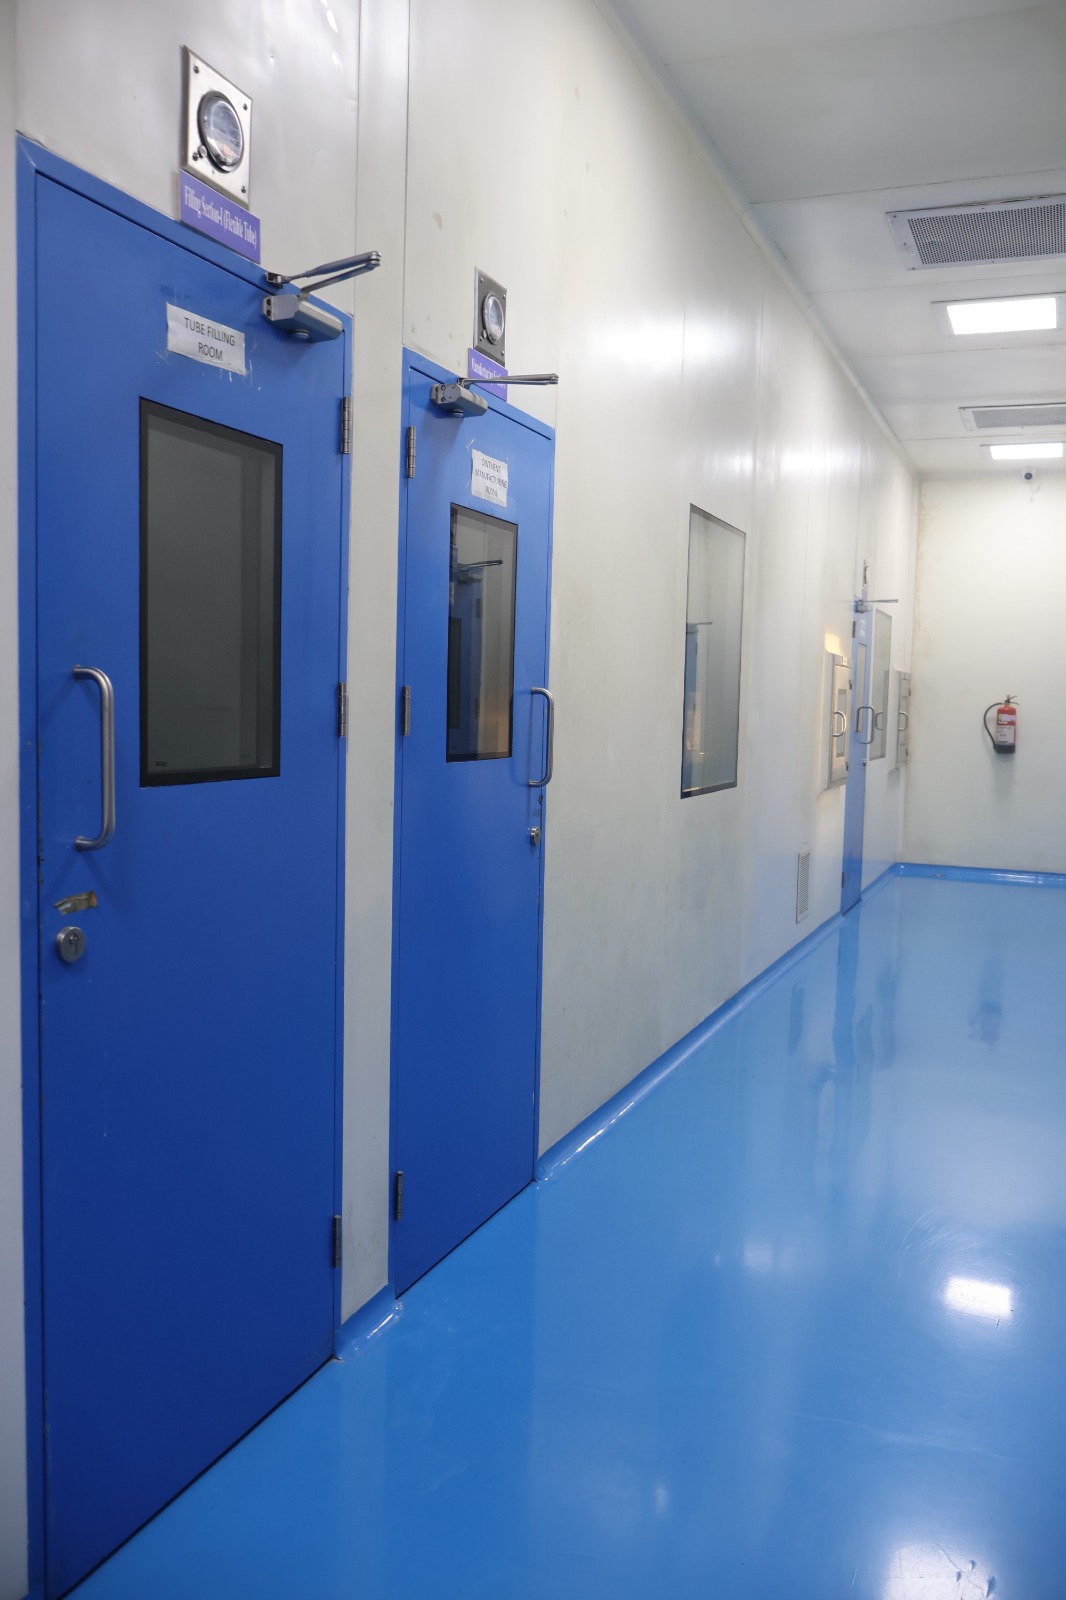 Contamination Barrier
Secondary differential pressure transition zone preventing foreign particle cross-transfer.
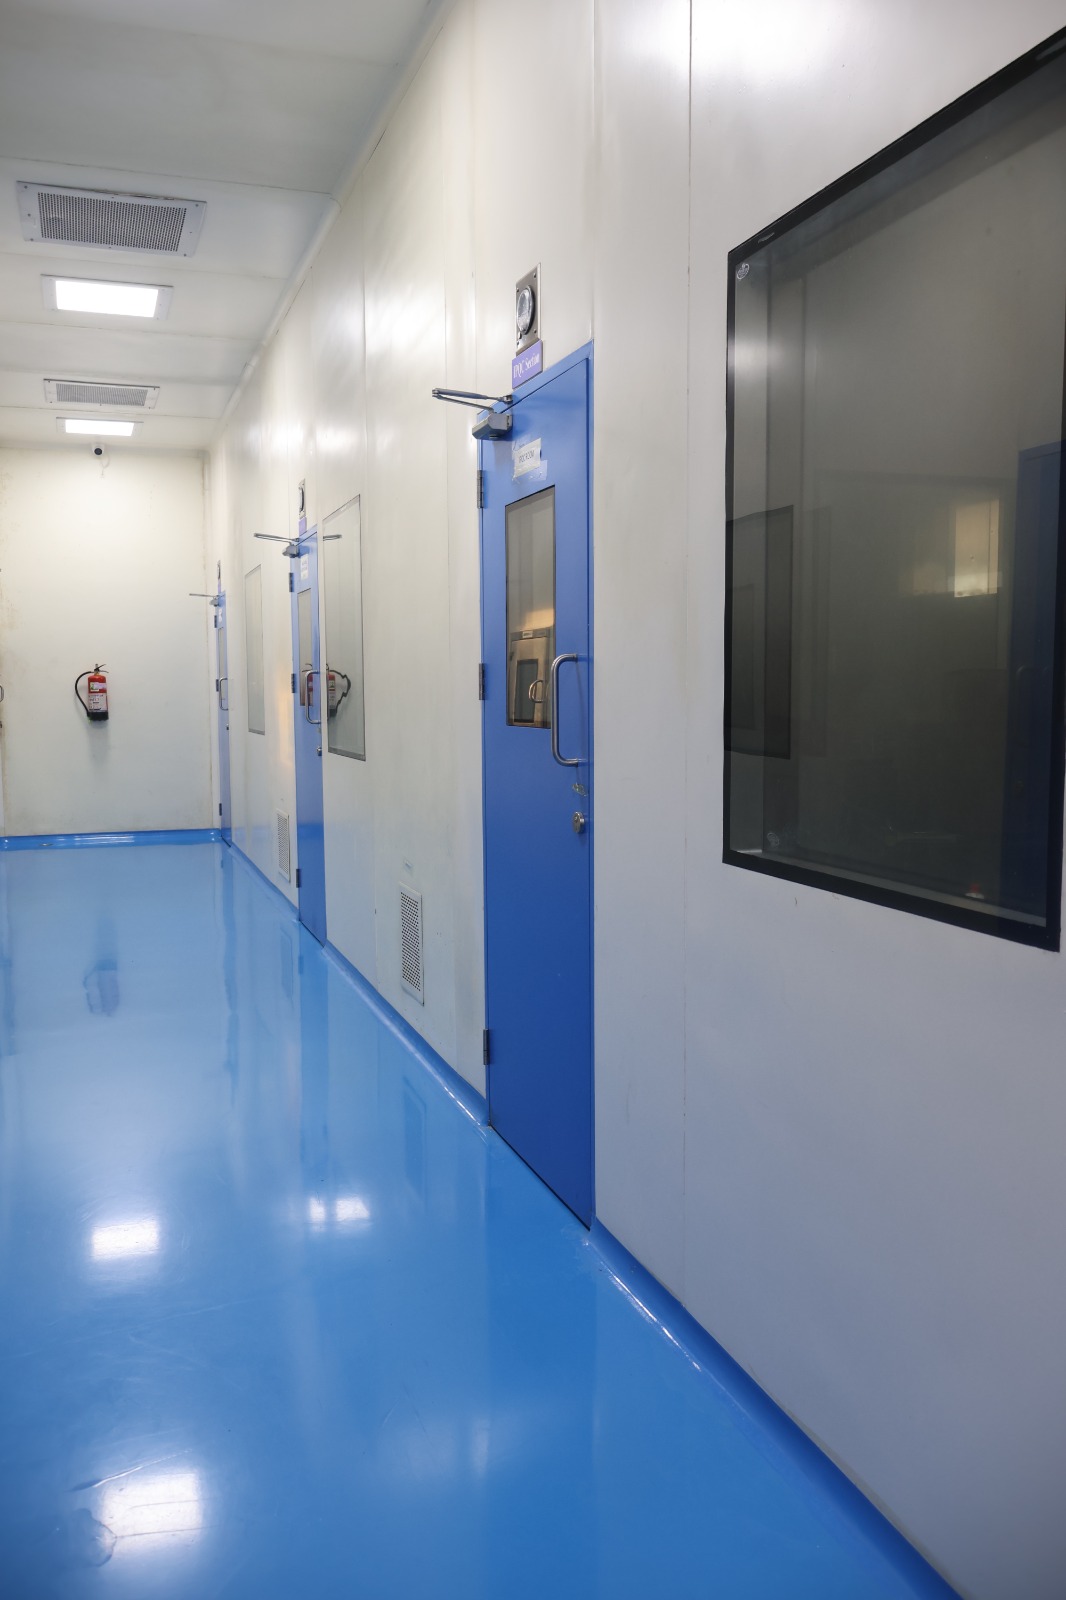 Sanitary Transit
Seamless epoxy-coated floors and cove wall junctions designed for sanitization protocols.
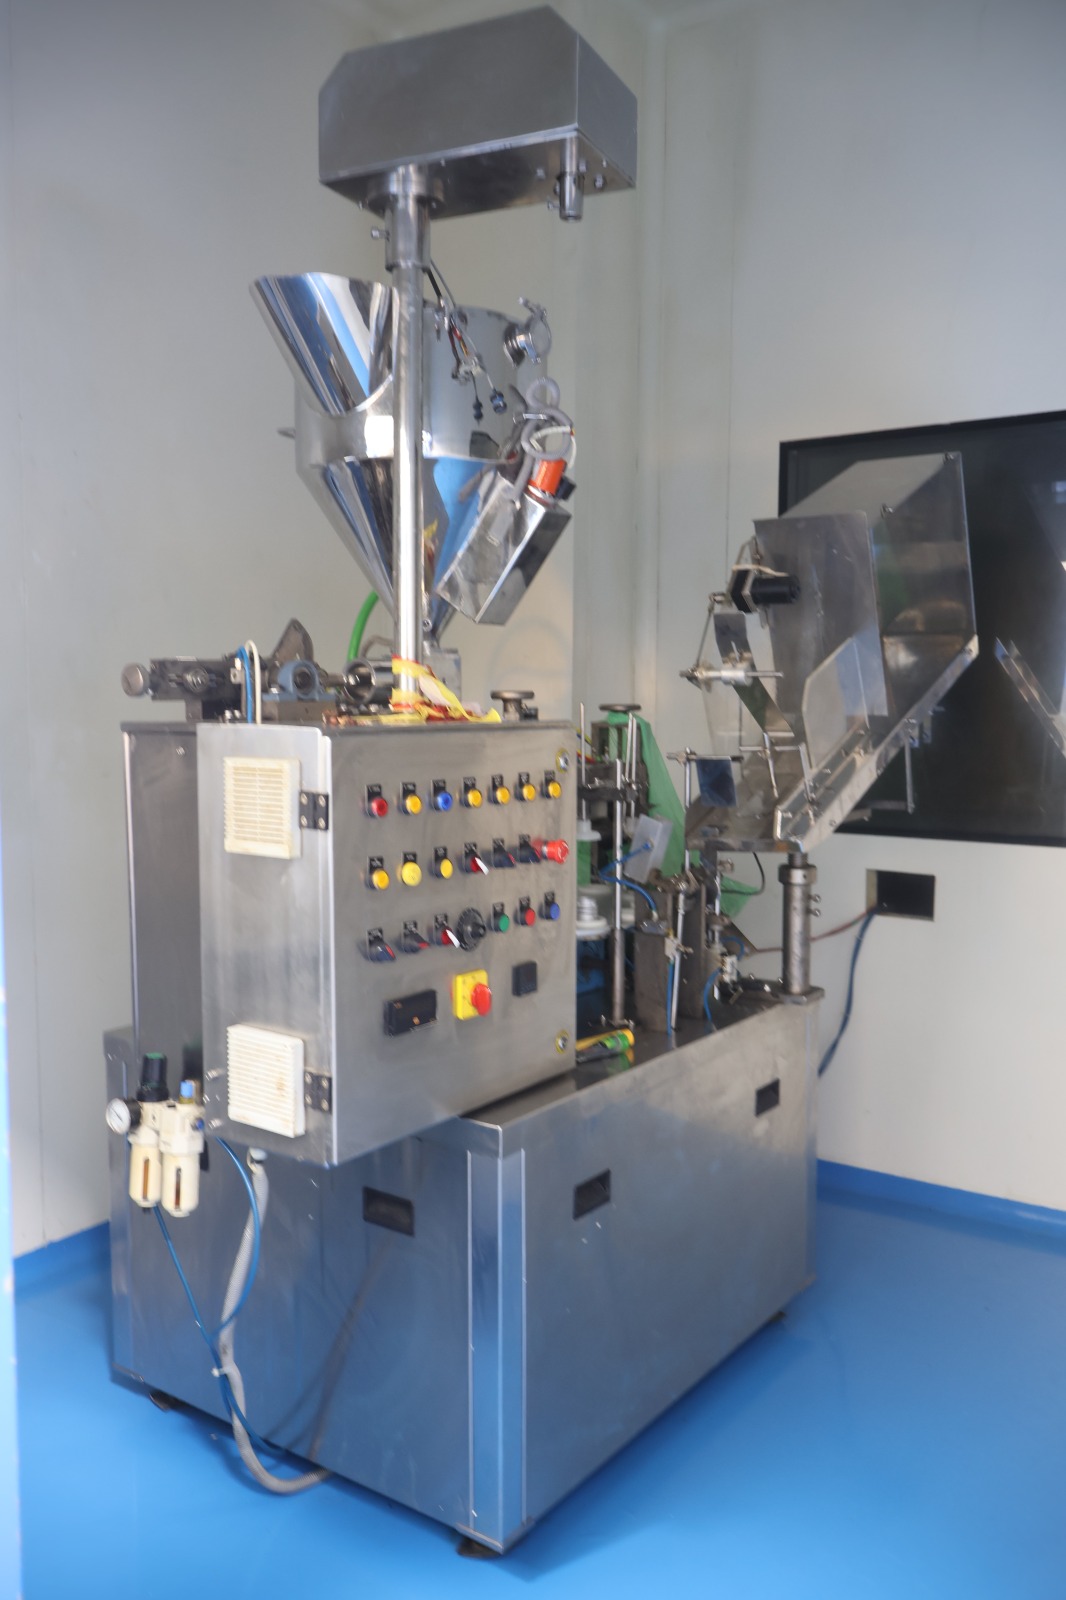 Tube Packaging
High-speed automatic rotary tube filling, sealing, trimming, and batch coding machine designed for airtight cosmetic tube production.
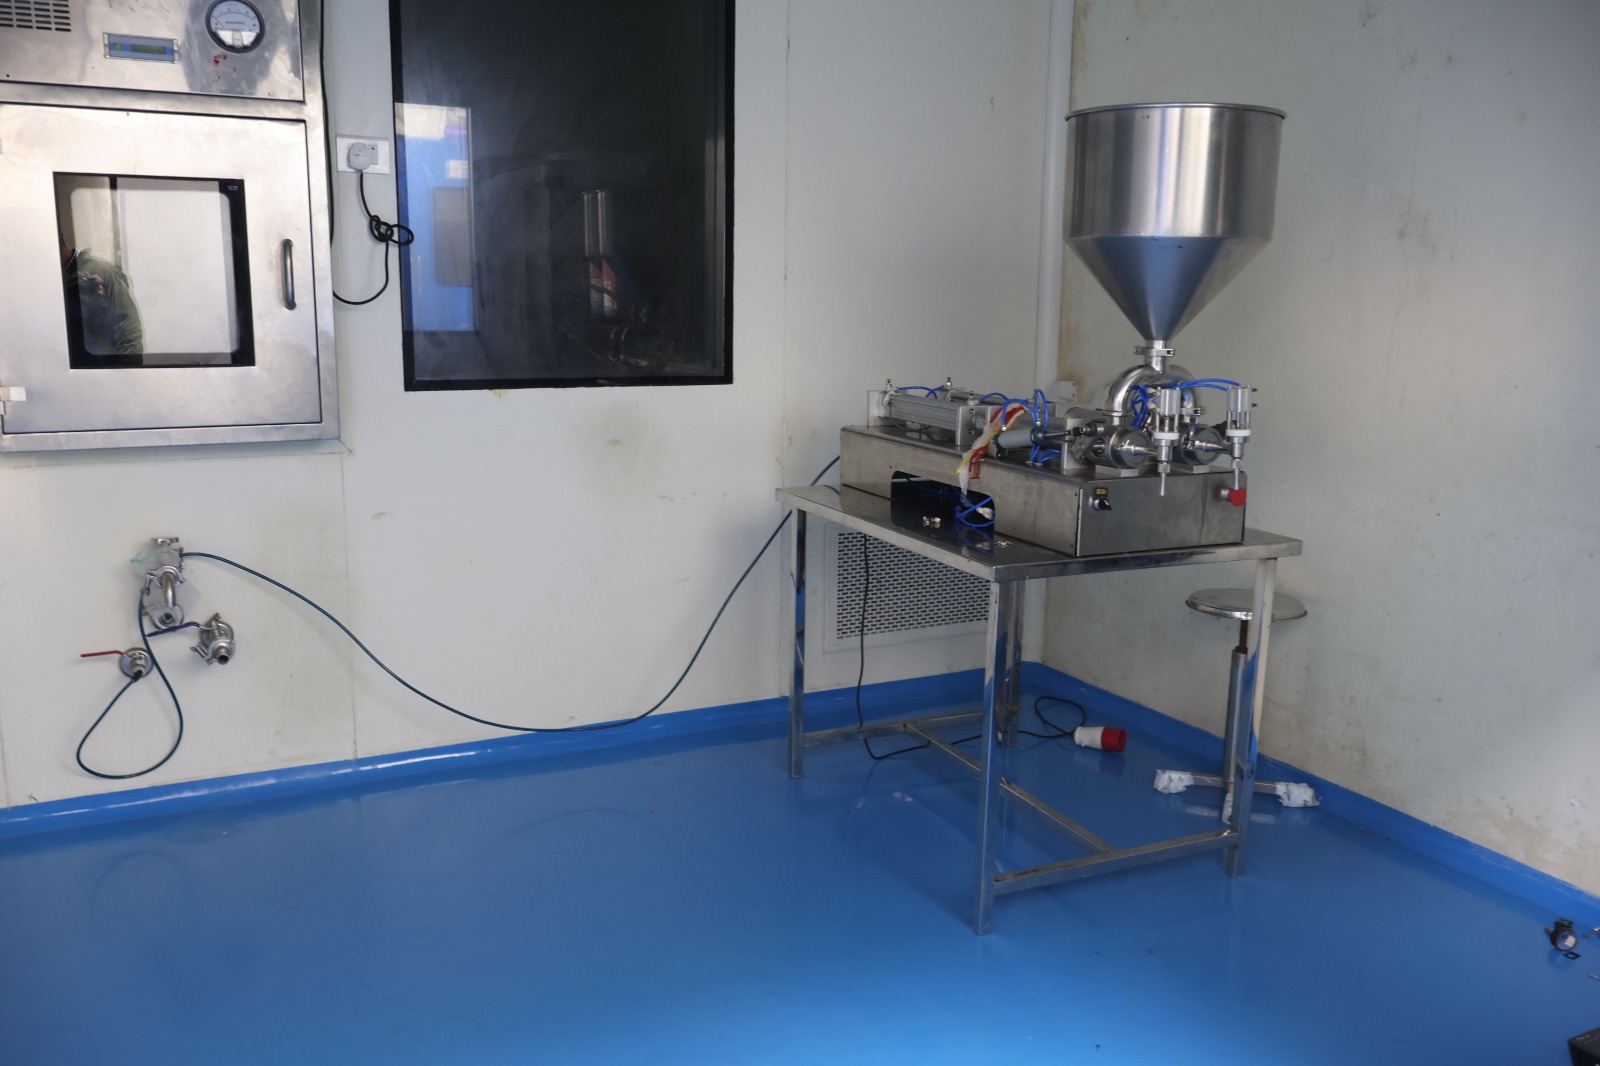 Packaging Automation
Dual-nozzle precision volumetric filling machine engineered for high-viscosity emulsions, gels, and restorative creams.
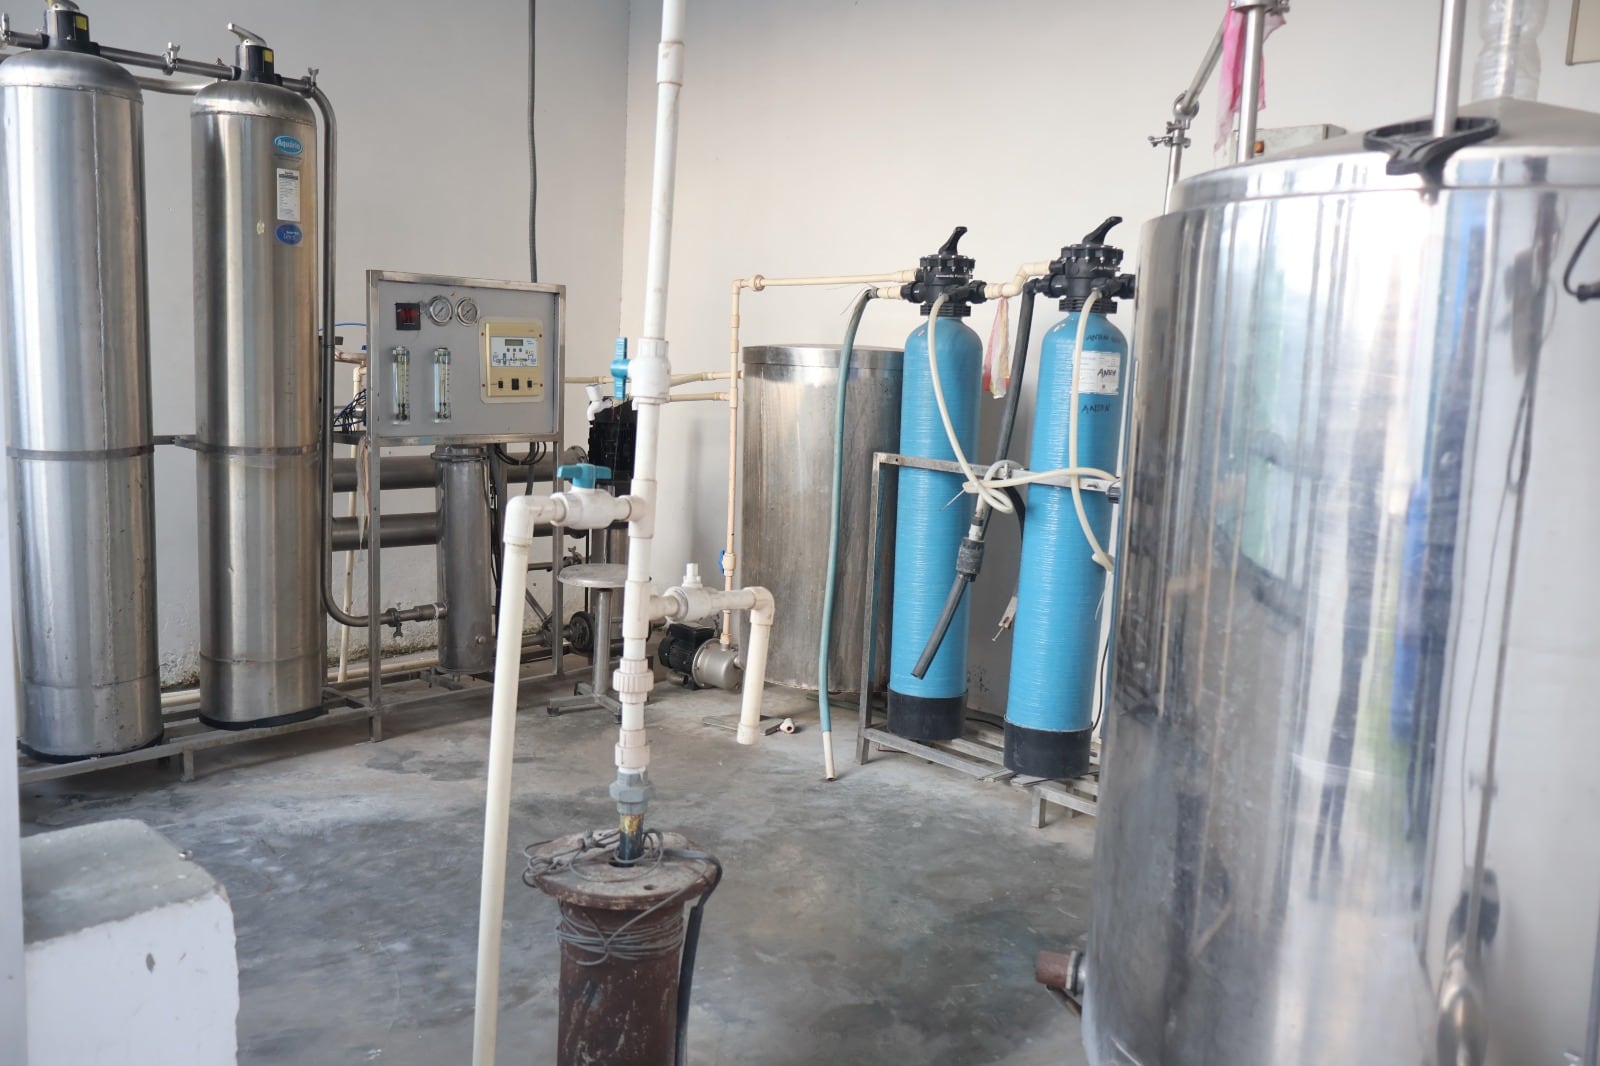 Water Purification
Industrial Reverse Osmosis Demineralized (RO DM) water treatment plant generating pharmaceutical-grade pure demineralized water for all formulation processes.
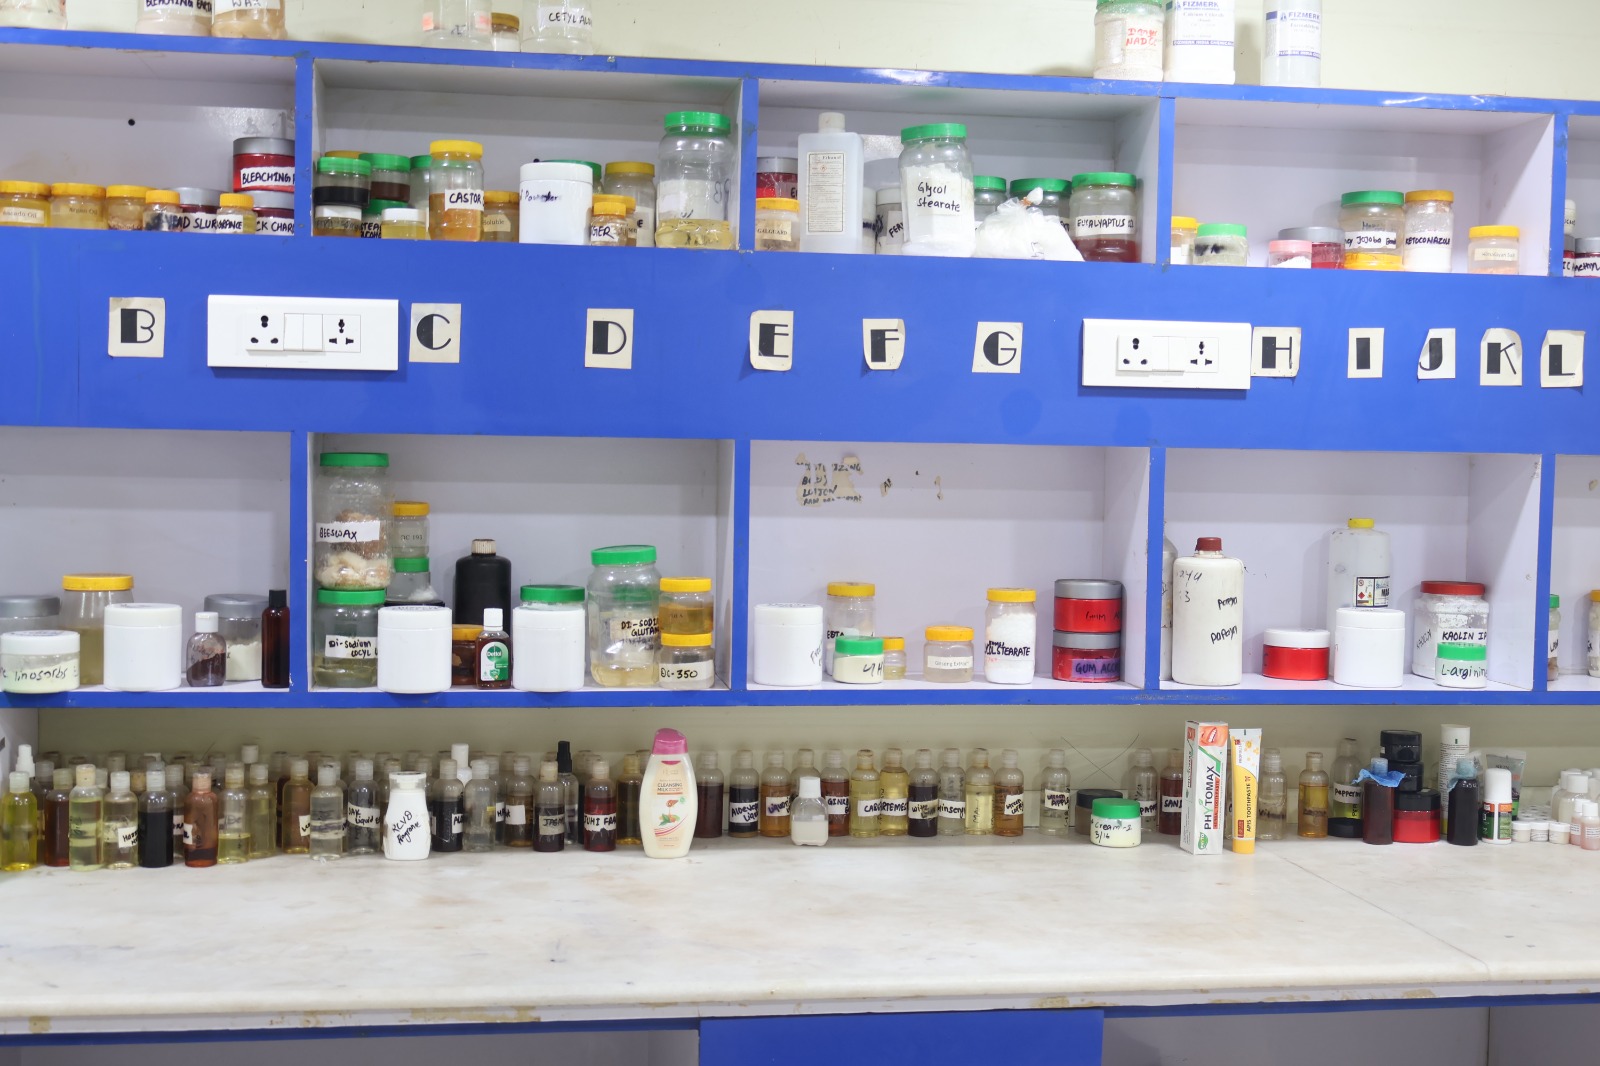 Sterility Testing
Thermal incubators monitoring bacterial and fungal growth for challenge preservation.
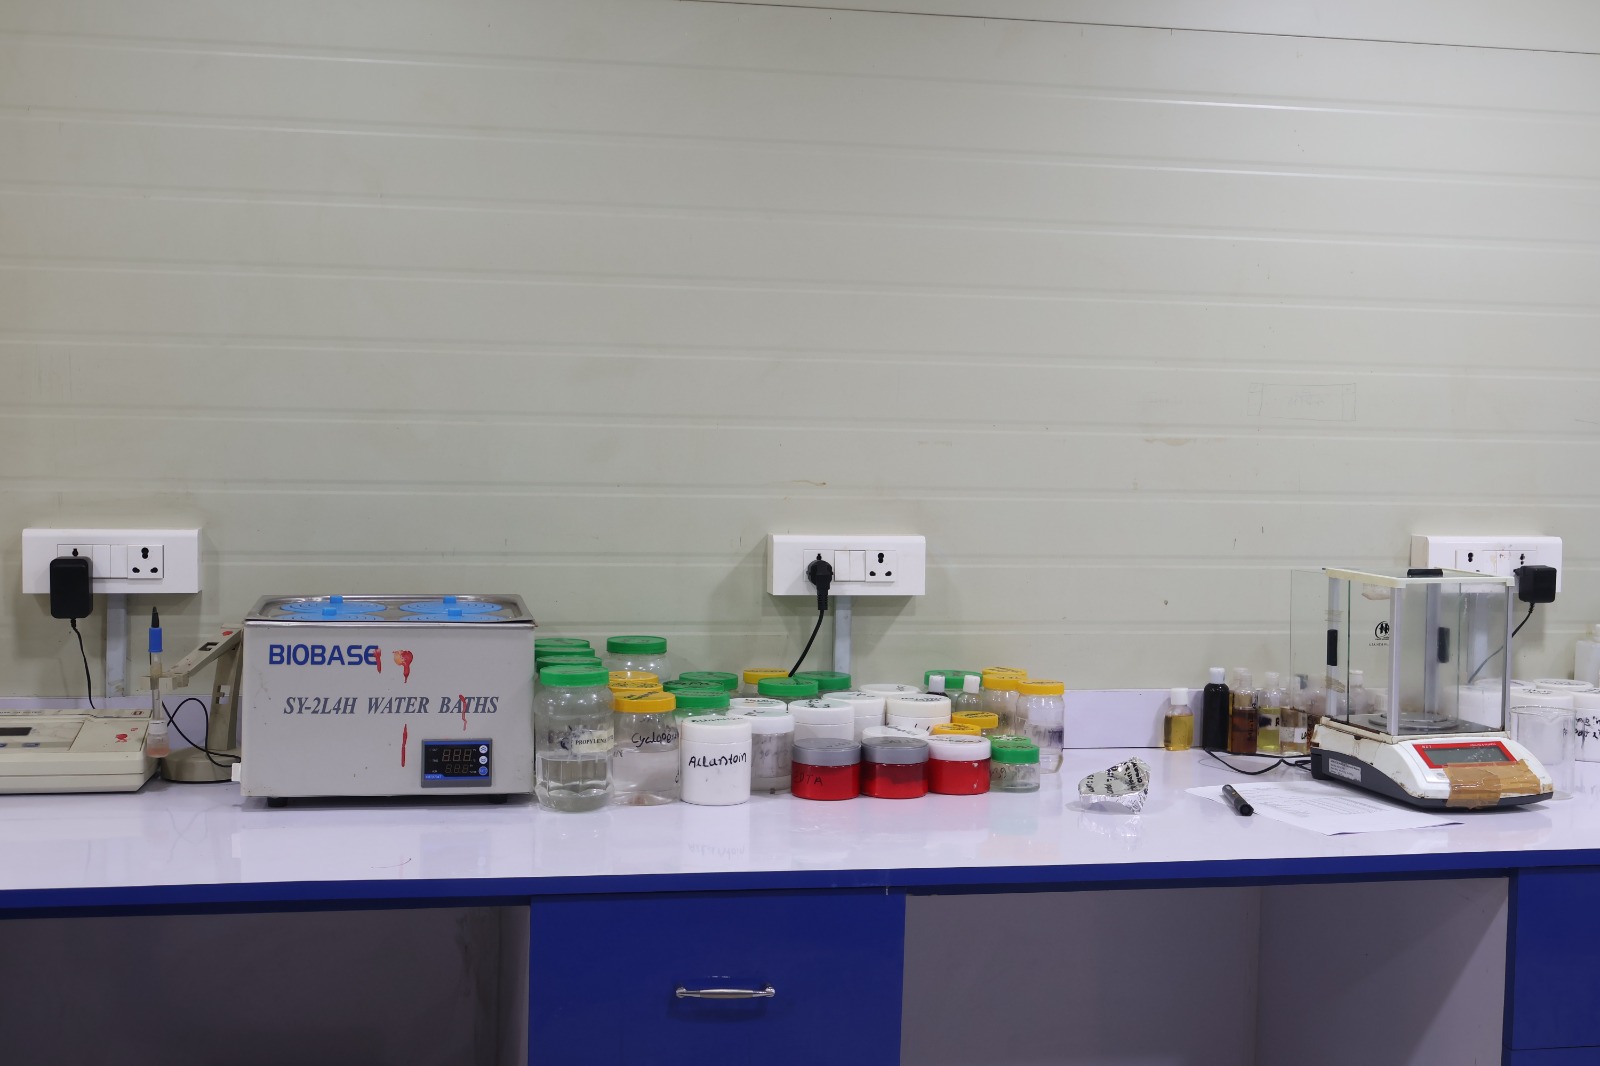 Formulation Science
Centrifugation and thermal stability testing verifying no phase separation.
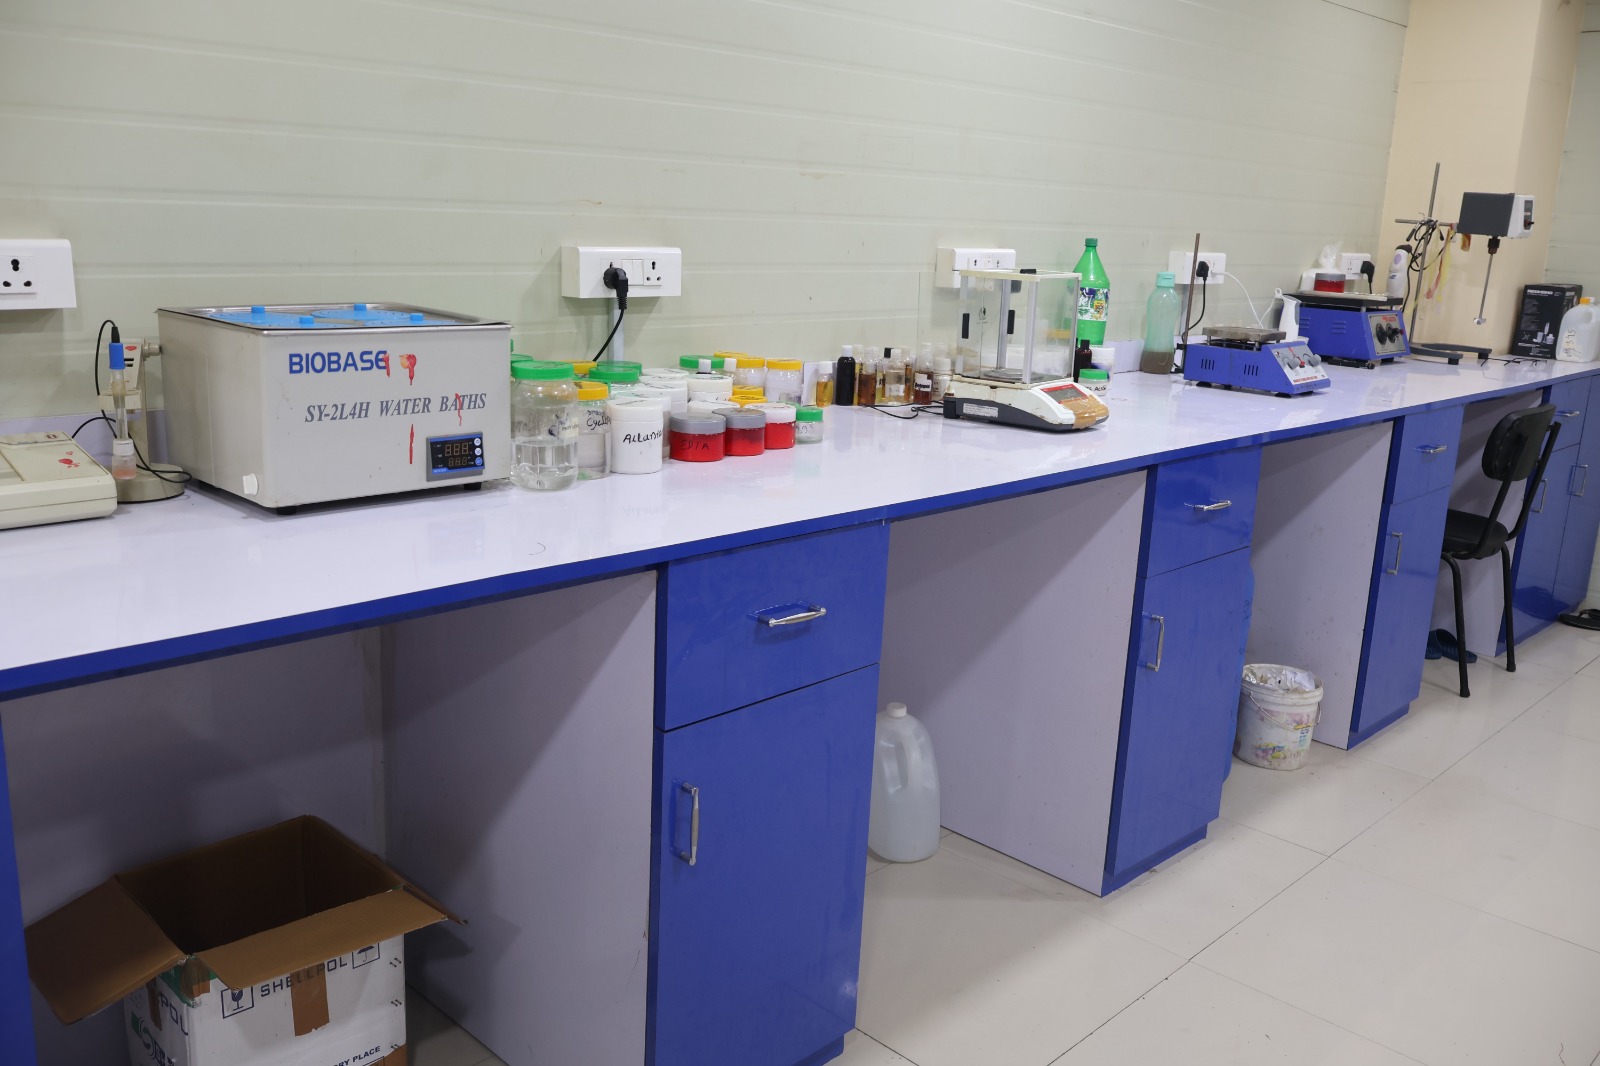 Active Dosing
Micro-analytical measurement benches for active ingredient calibration.
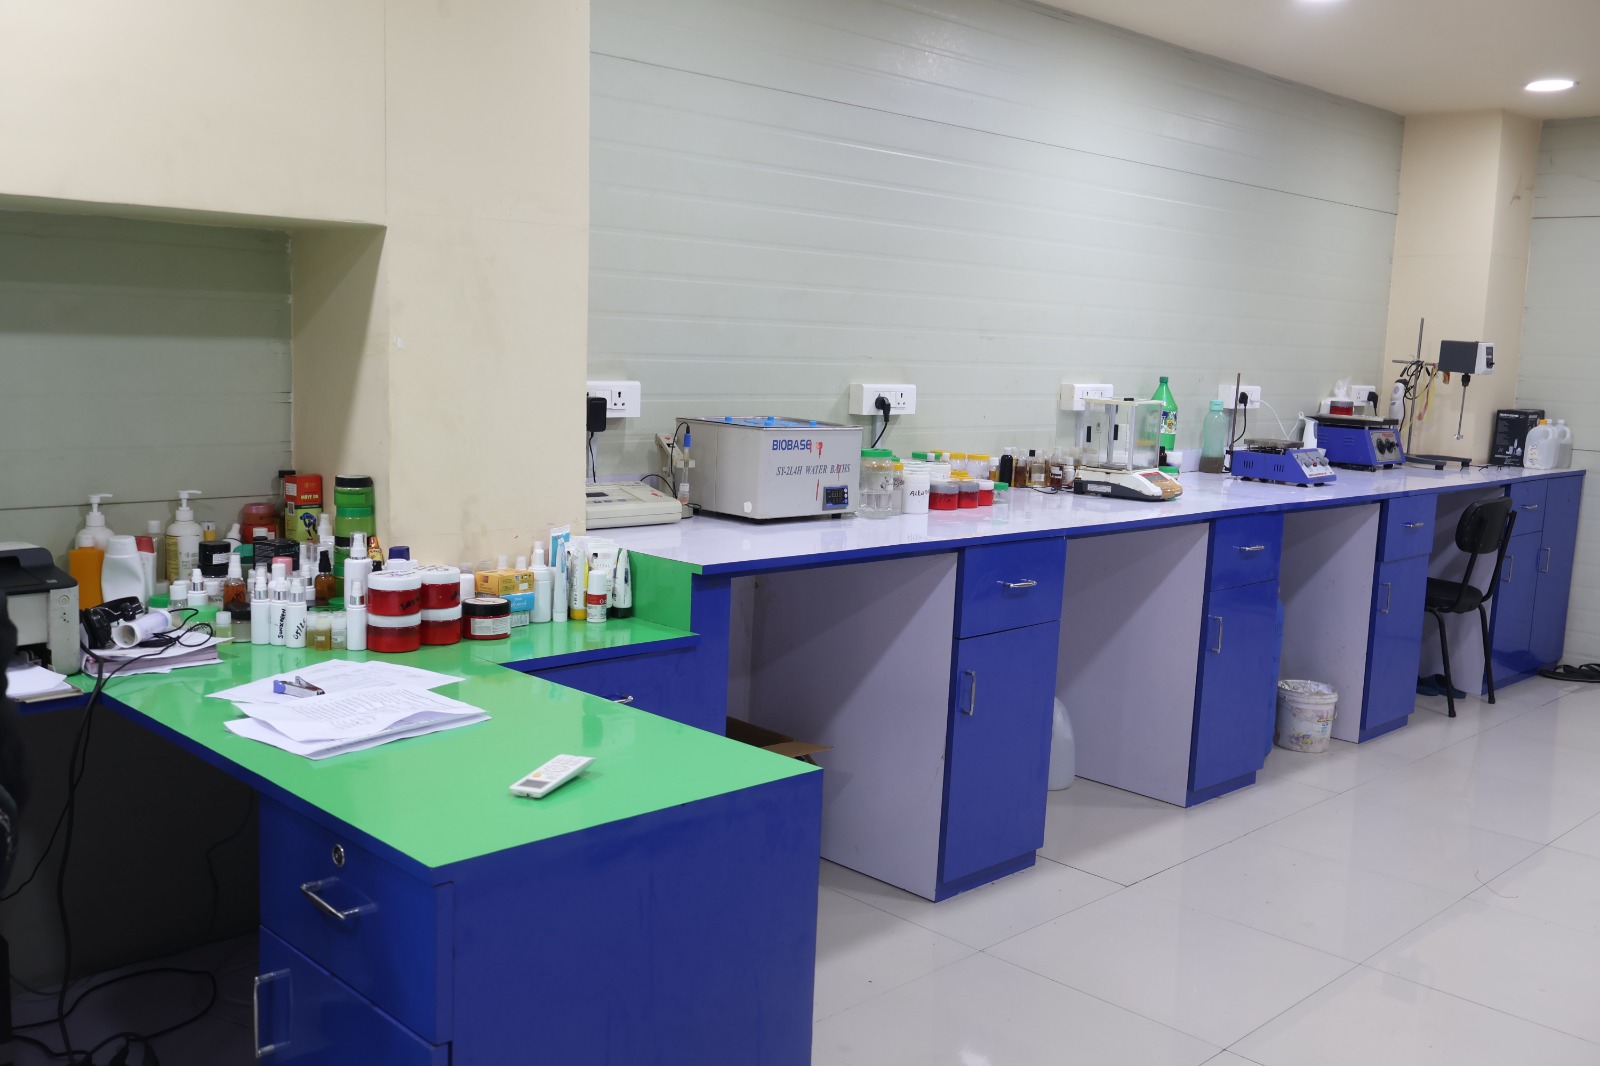 Regulatory Records
Temperature and humidity-controlled archive housing batch retention samples.
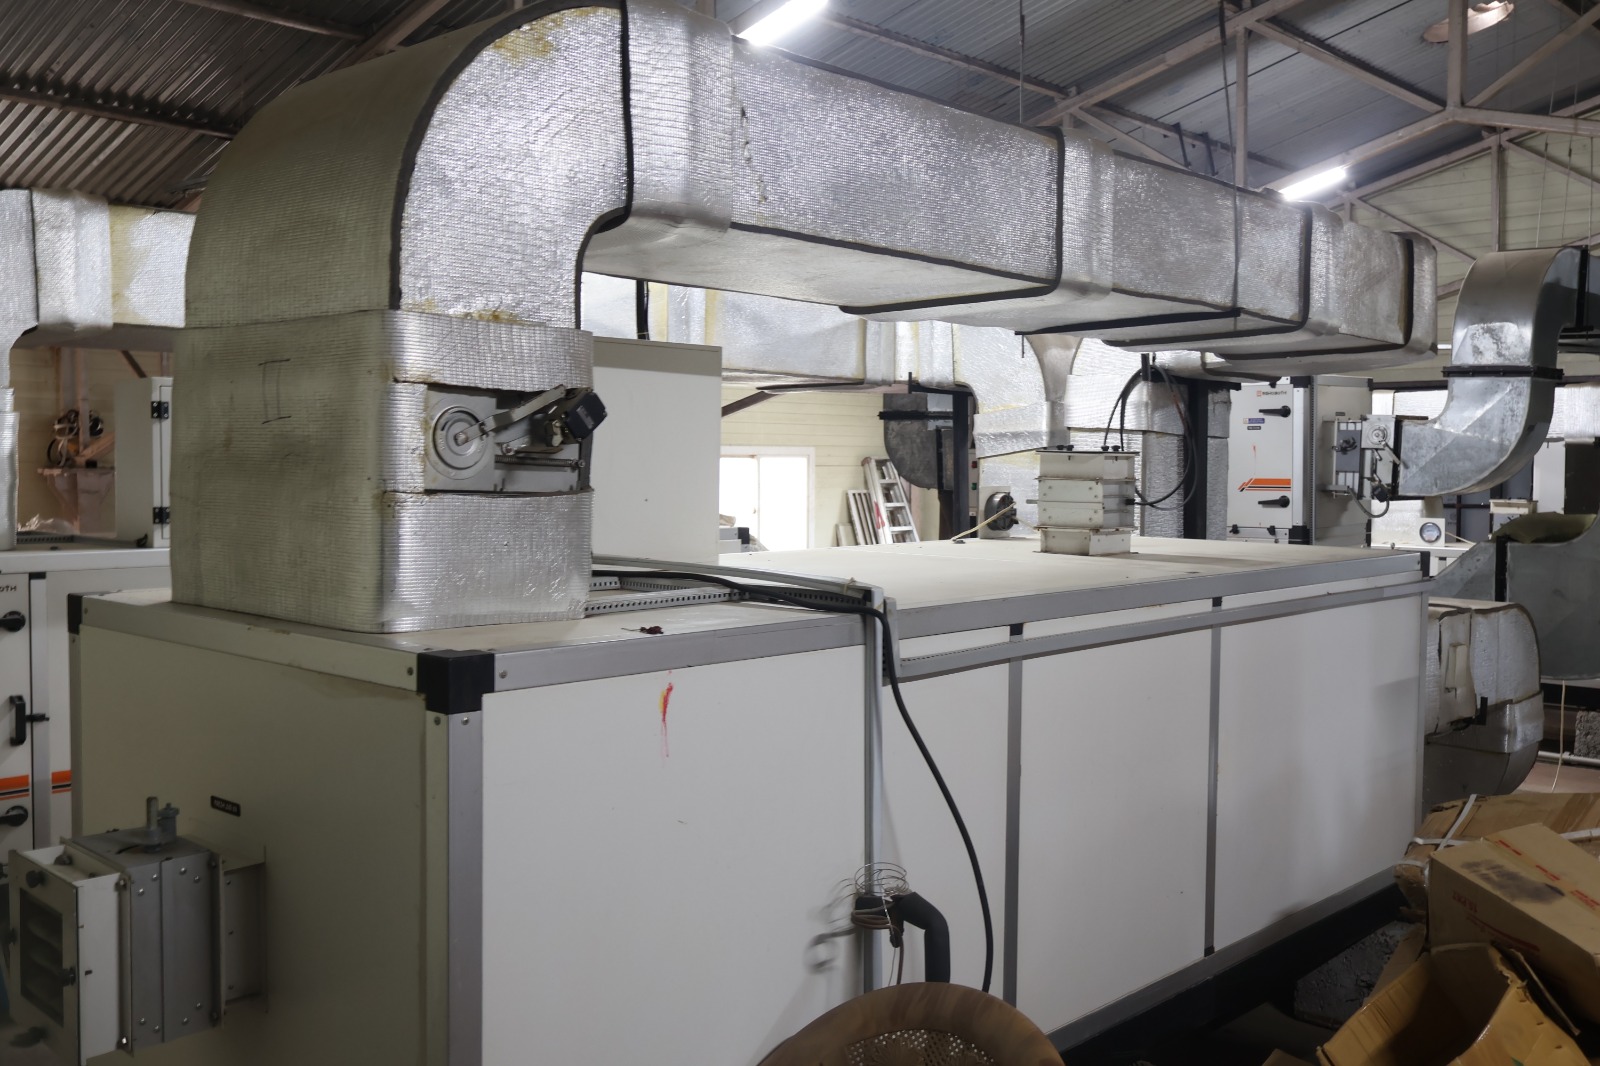 HVAC Engineering
Centralized Air Handling Units maintaining negative atmospheric pressure, temperature regulation, and continuous particulate filtration.
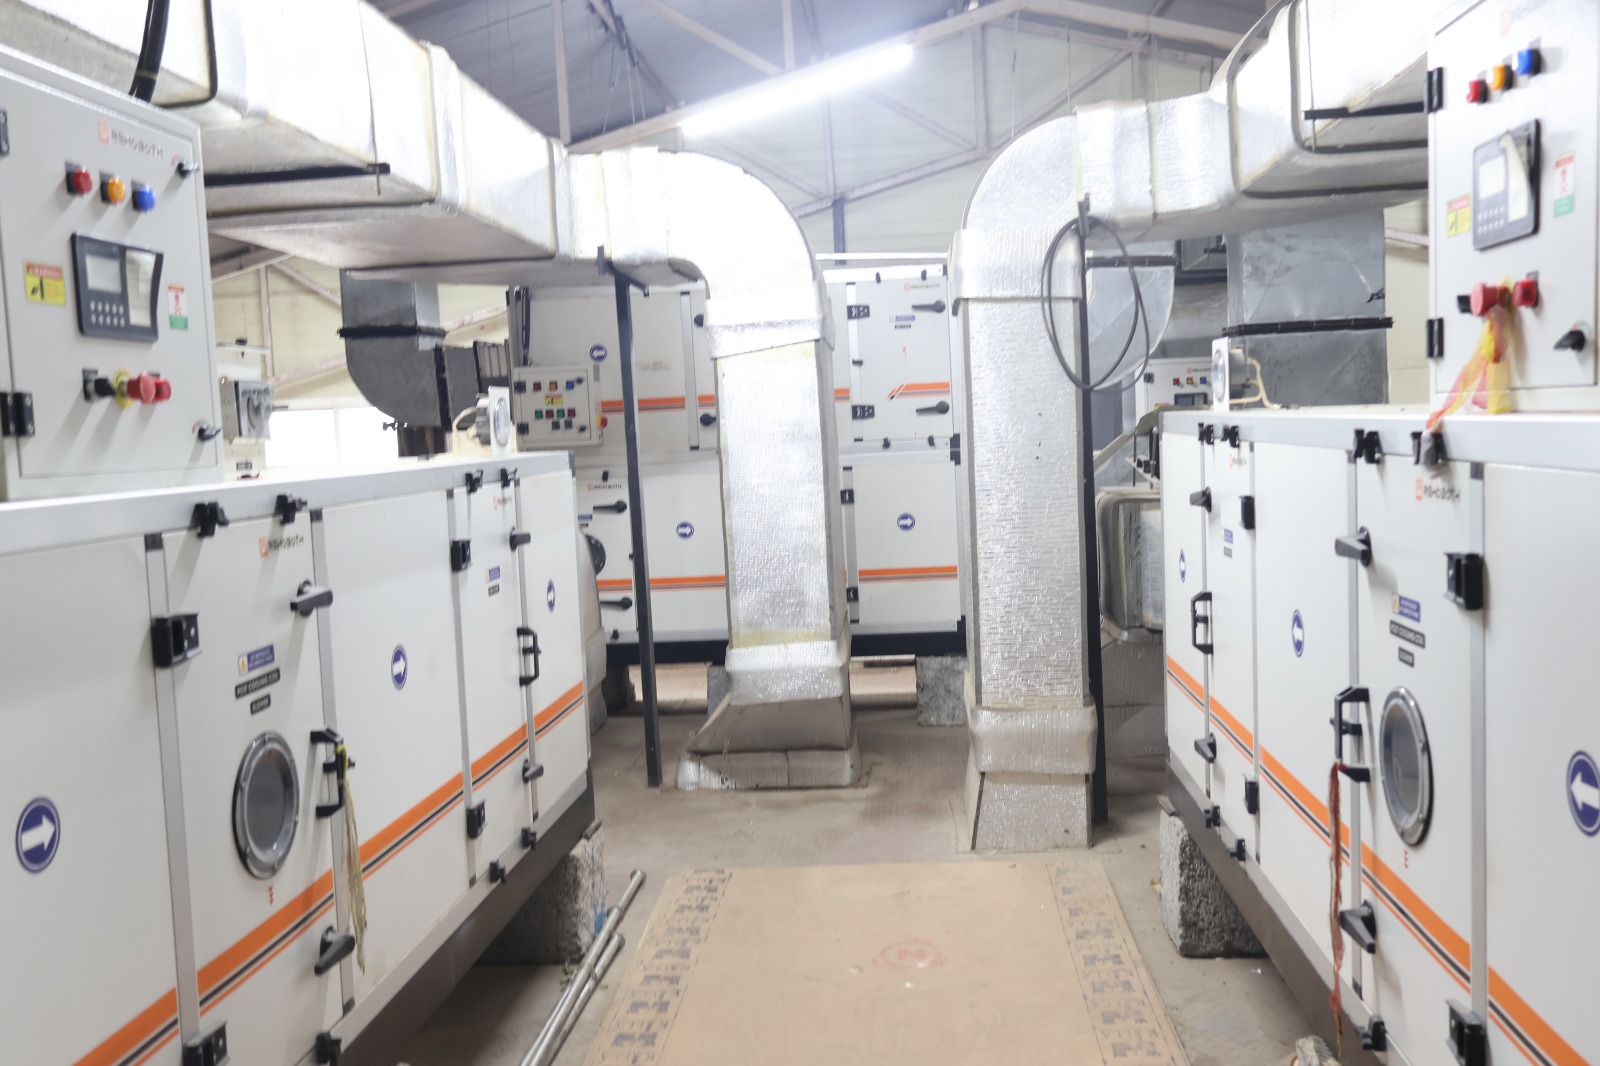 Air Quality Control
Multi-stage HEPA filtration module delivering continuous filtered air exchanges per hour.
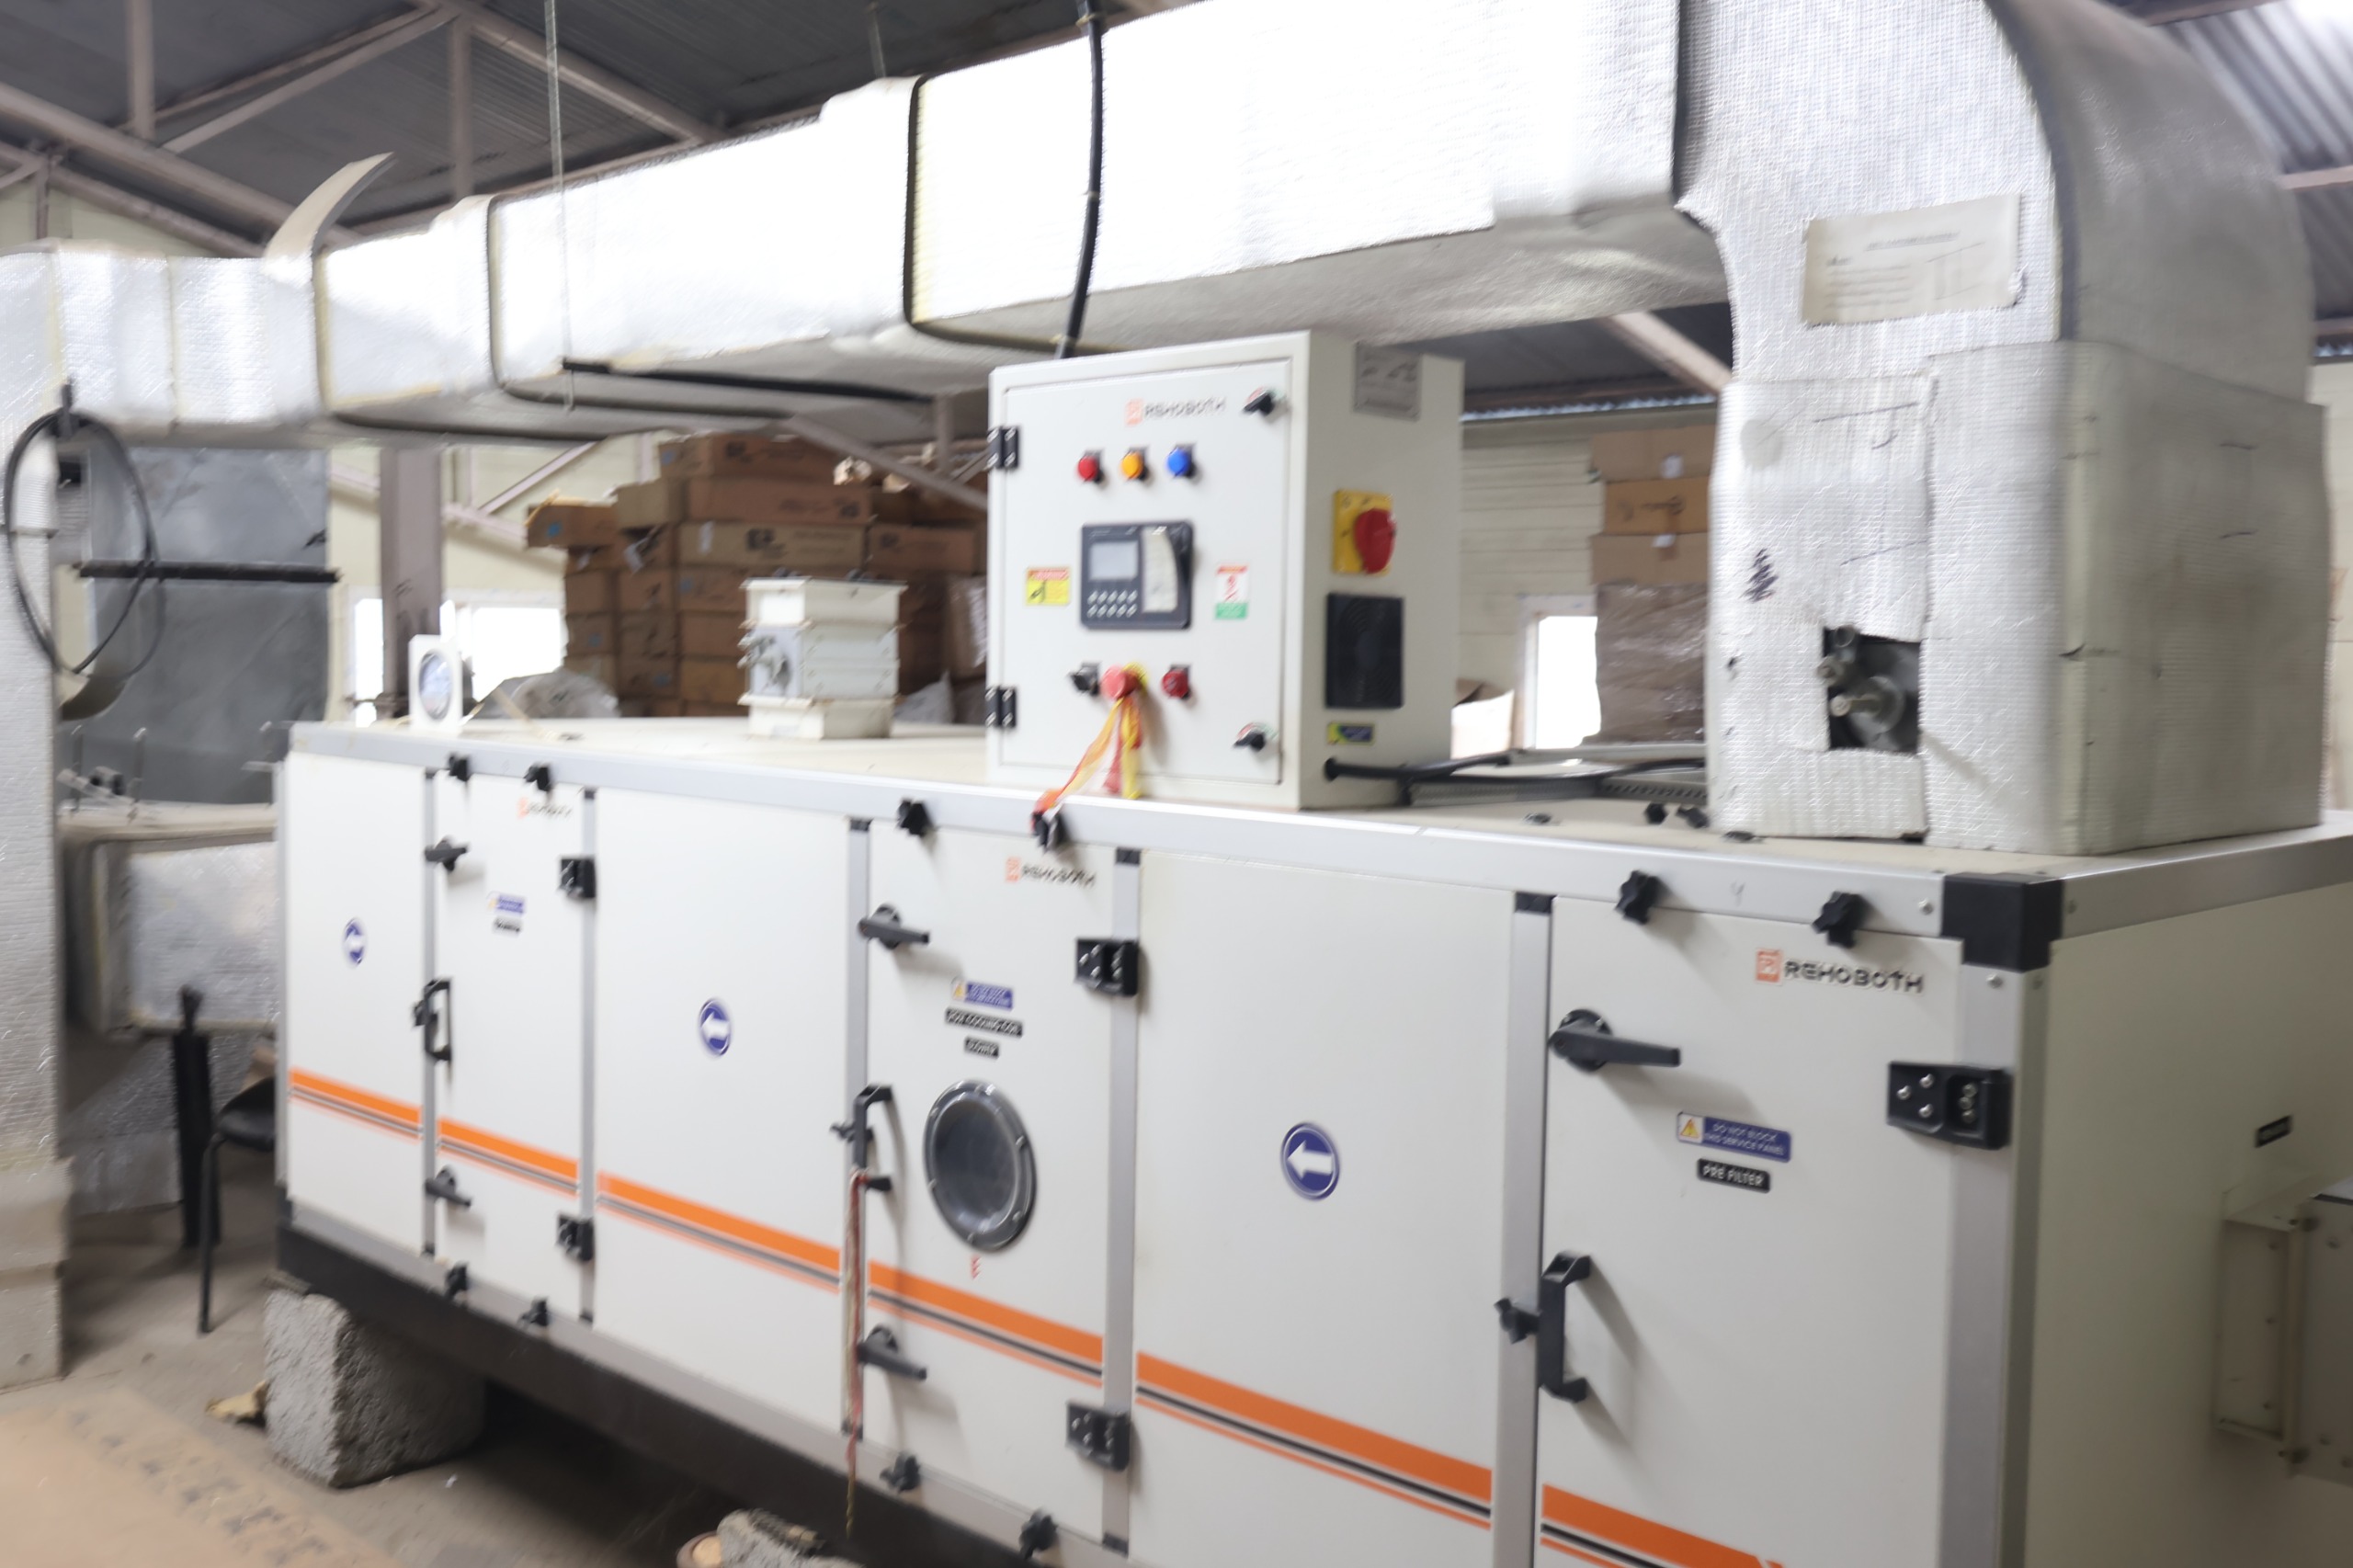 Environmental Control
Dedicated clean air distribution unit for R&D laboratories and analytical testing suites.
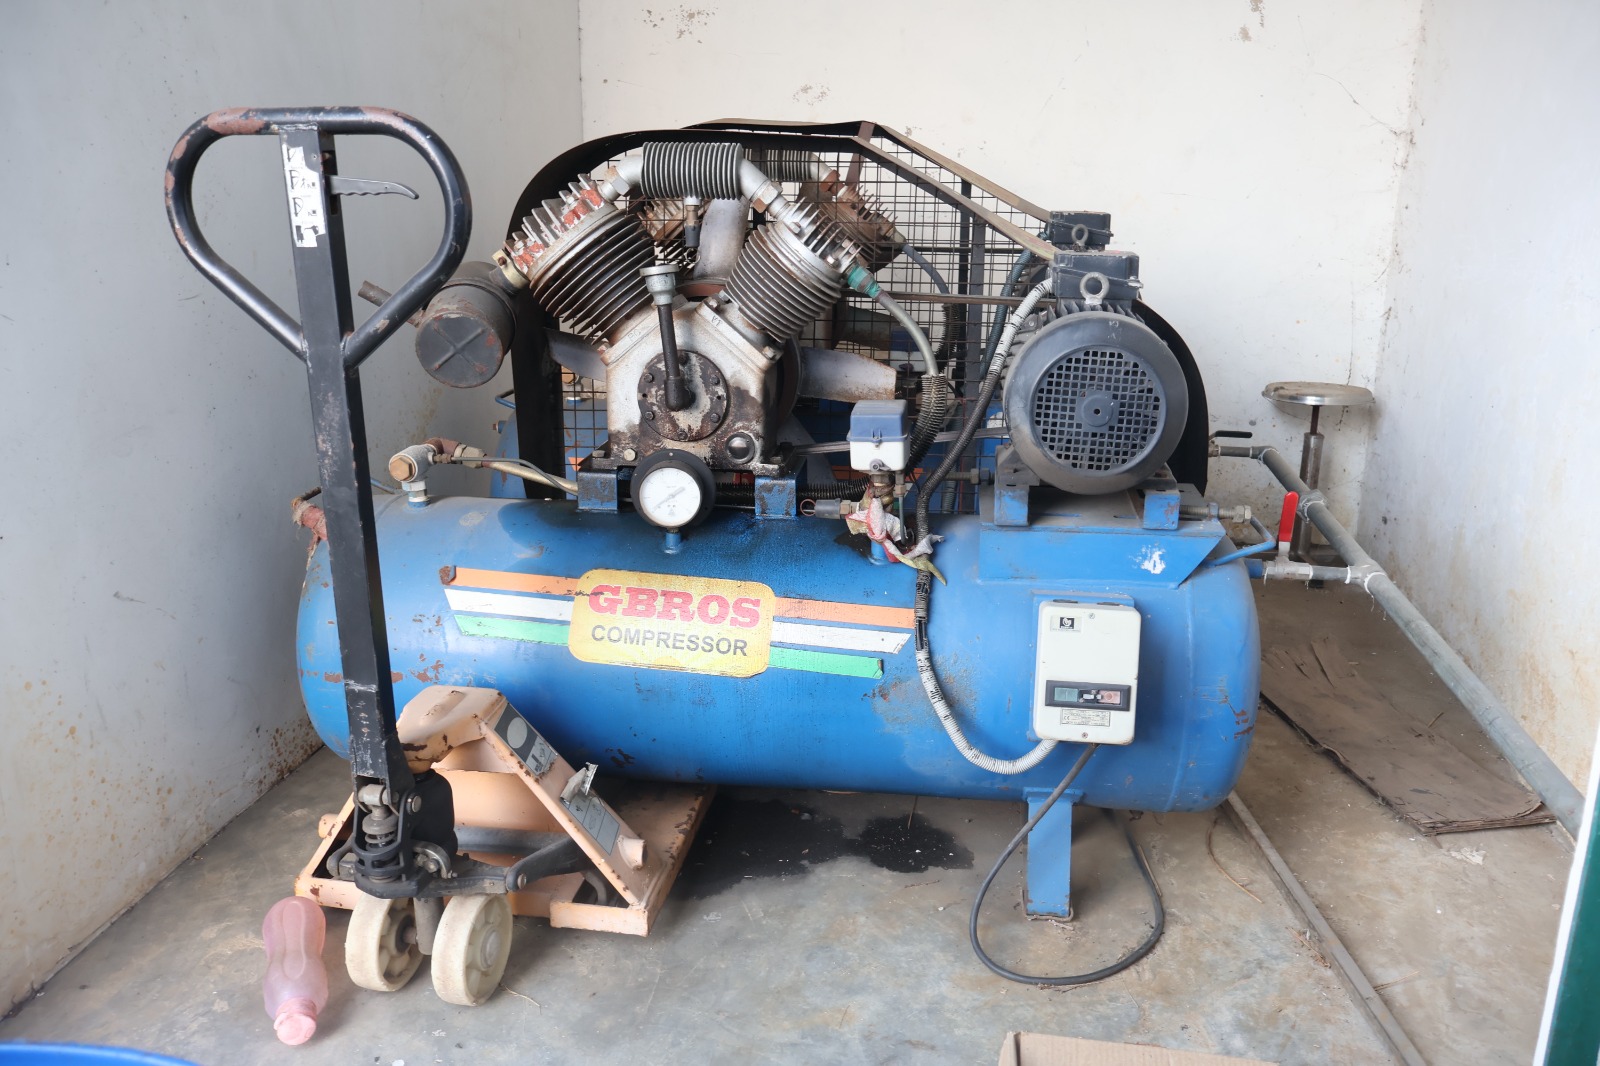 Pneumatic Utility
Oil-free medical grade compressed air power plant driving all automated packaging lines.
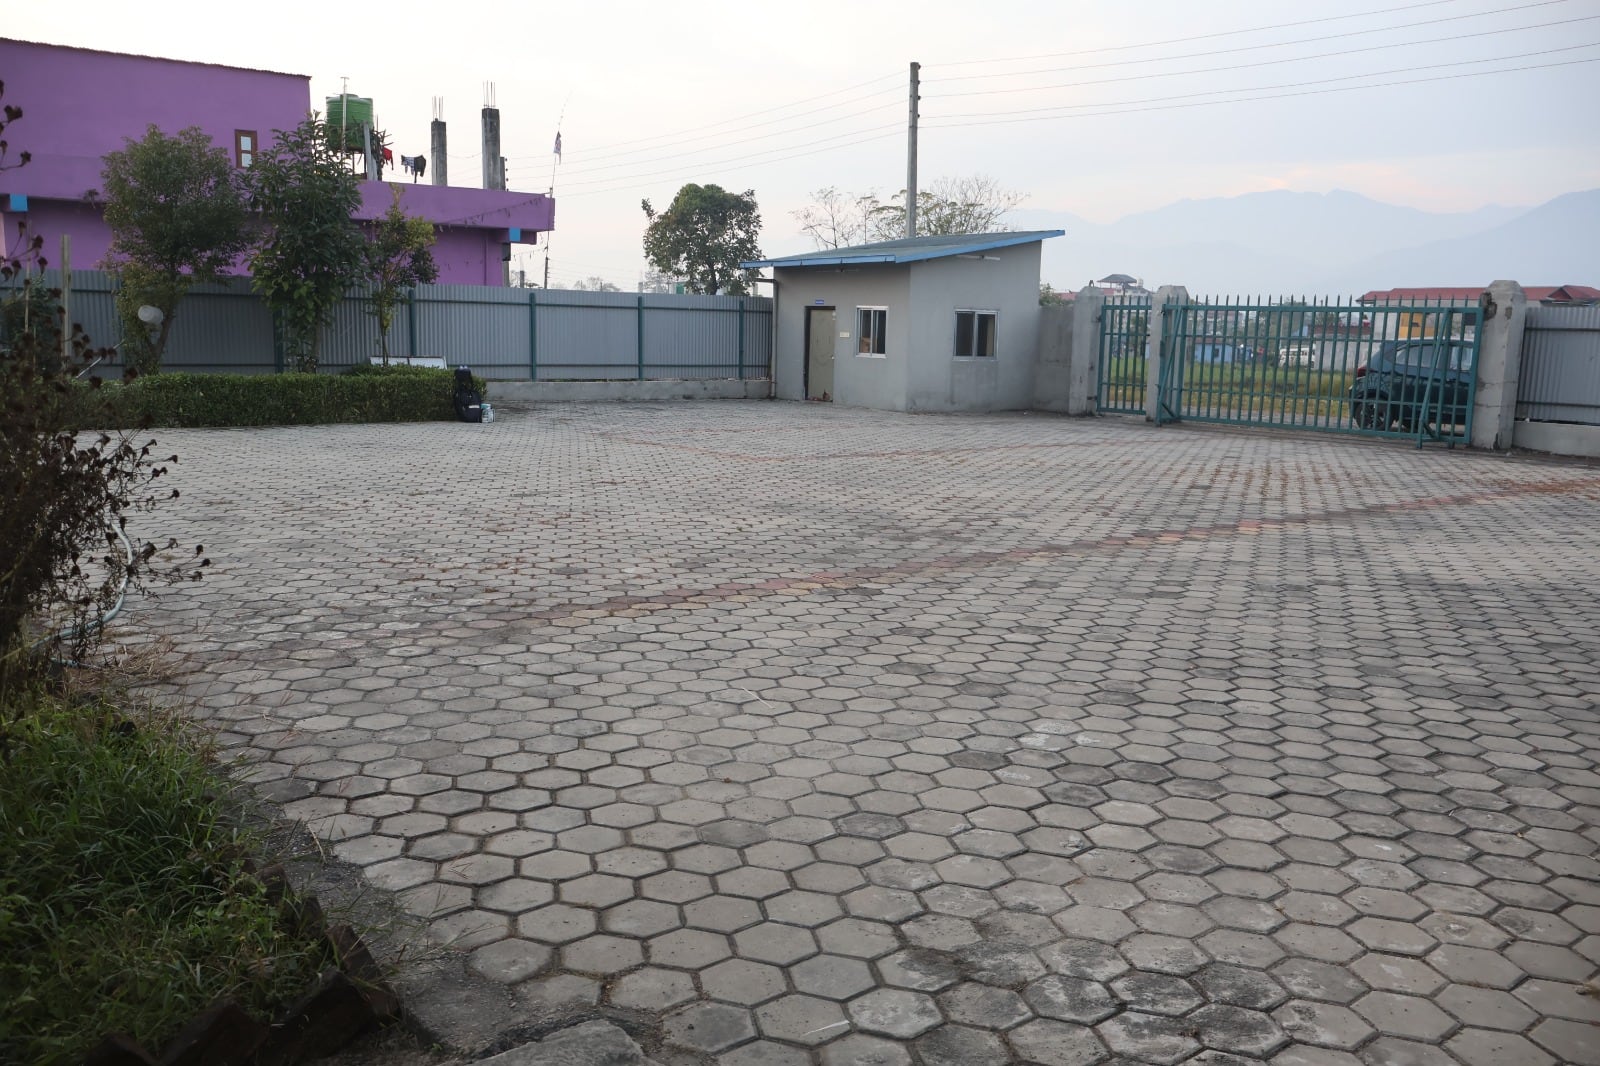 Logistics Hub
Dedicated truck loading bays and raw material delivery security gates.
Phytomax Care Pvt. Ltd. — Direct Verification & Communication Desk