"Adding Value to Life in Beauty and Skin Care Science"
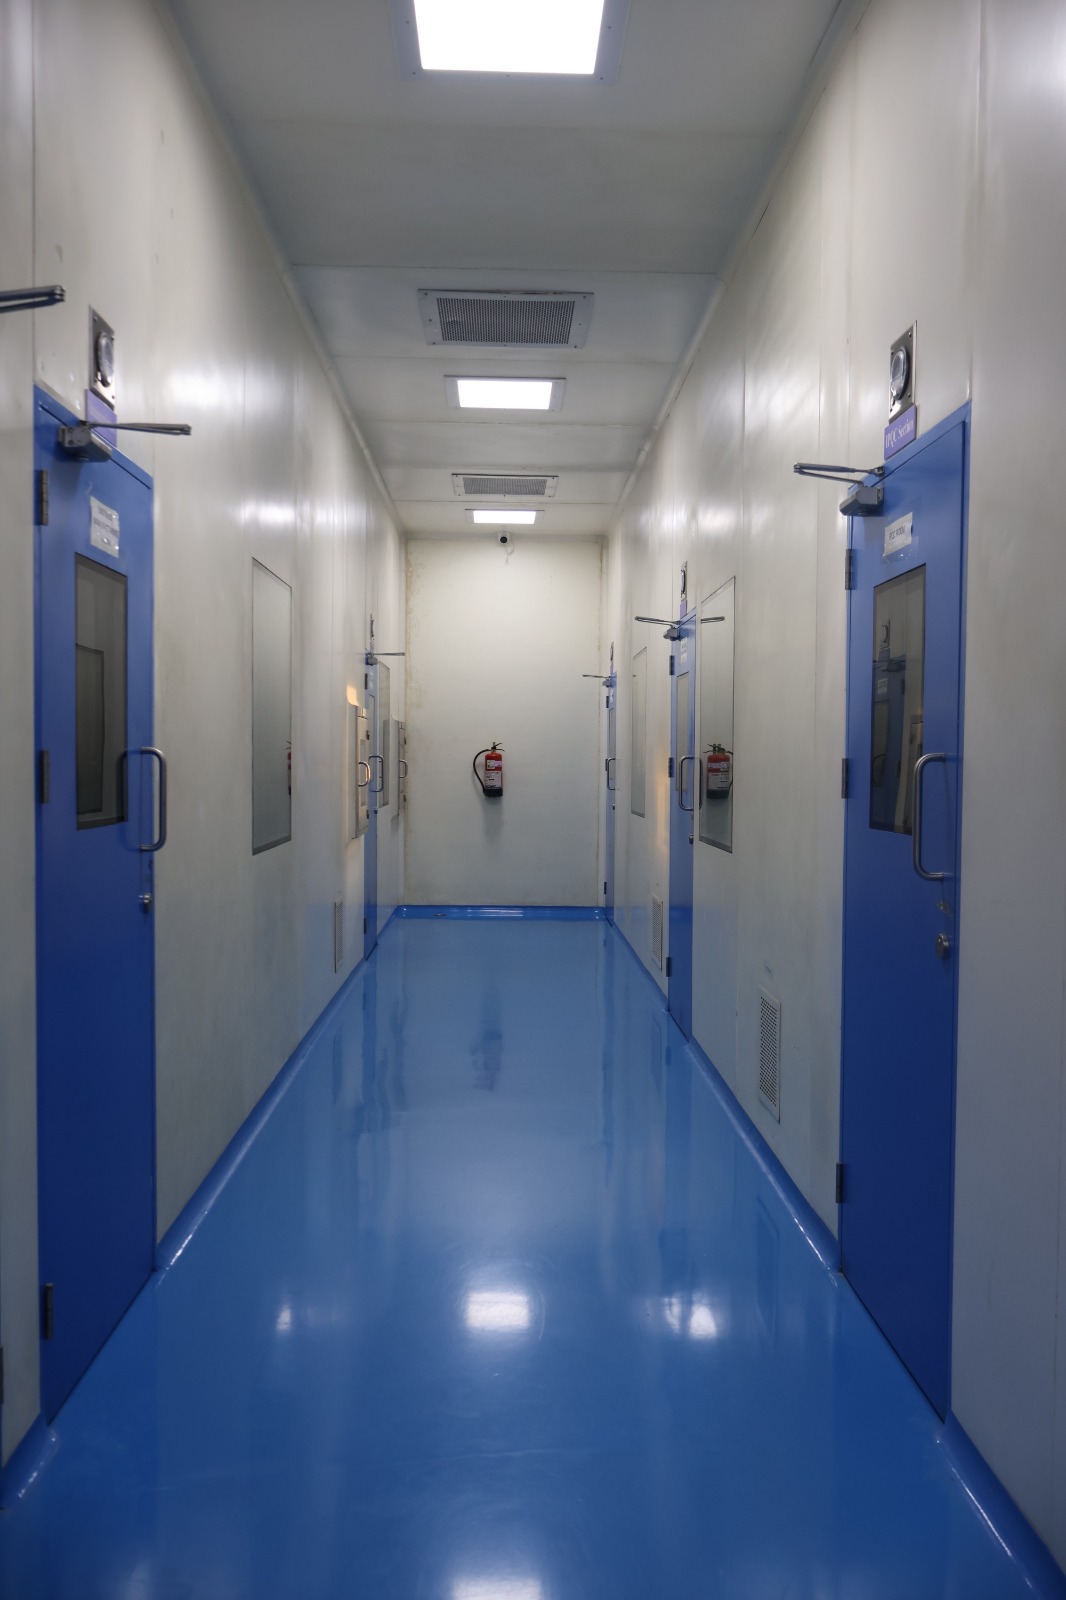
Our operational mandate prioritizes verified safety, multi-stage RO demineralized water purity, HEPA air conditioning, and batch consistency over marketing embellishment.
Every active concentration is benchmarked against published scientific literature and proven dermatological efficacy thresholds.
We pair biocompatible lipid matrices (ceramides, squalane, amino acids) with responsibly harvested botanicals suitable for South Asian skin types.
Zero unnecessary synthetic dyes, parabens, harsh sulfates, or deceptive claims. Formulations pass stringent stability and challenge tests.
All ingredients and labeling comply with the Department of Drug Administration (DDA) cosmetic frameworks and national consumer safety standards.
High-purity water is the primary carrier matrix for topical dermocosmetics and skin-barrier emulsions. Phytomax Care operates a dedicated industrial Reverse Osmosis Demineralized (RO DM) water treatment plant, combining multi-stage resin deionization, dual-pass RO membranes, and inline UV sterilization for total microbiological and chemical purity.
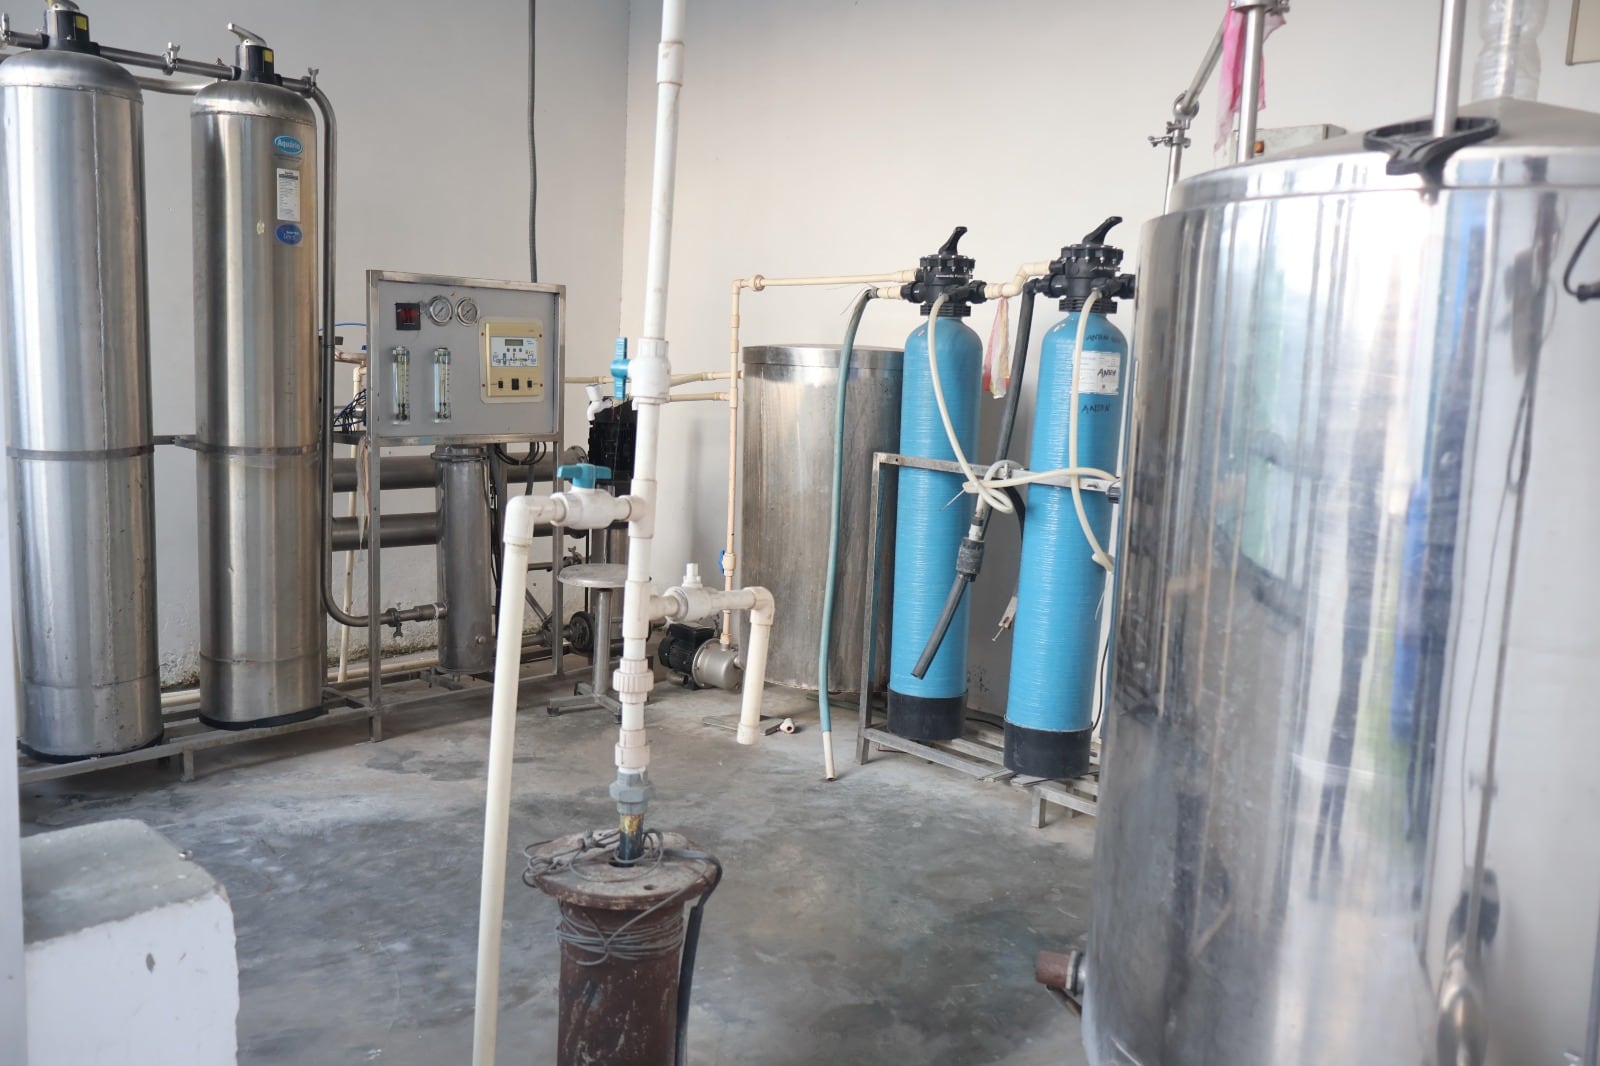
Raw source water undergoes sand filtration, activated carbon adsorption, ion-exchange demineralization (DM), and reverse osmosis to eliminate dissolved mineral ions, heavy metals, and particulate impurities.
Demineralized water is continuously recirculated through electro-polished 316L stainless steel piping loops at high turbulent velocity to prevent stagnant dead-legs and biofilm colonization.
In-house microbiologists and analytical chemists test daily samples from multiple loop valves to verify total dissolved solids (TDS), pH calibration, and complete absence of microbial endotoxins.
Atmospheric particulate control is the backbone of sterile skincare manufacturing. Phytomax Care maintains dedicated heavy-duty AHU infrastructure maintaining negative pressure cascades from cleanroom compounding suites to exterior corridors. Atmospheric particulate control is the backbone of sterile skincare manufacturing. Phytomax Care maintains dedicated heavy-duty AHU infrastructure maintaining positive pressure cascades from cleanroom compounding suites to exterior corridors.
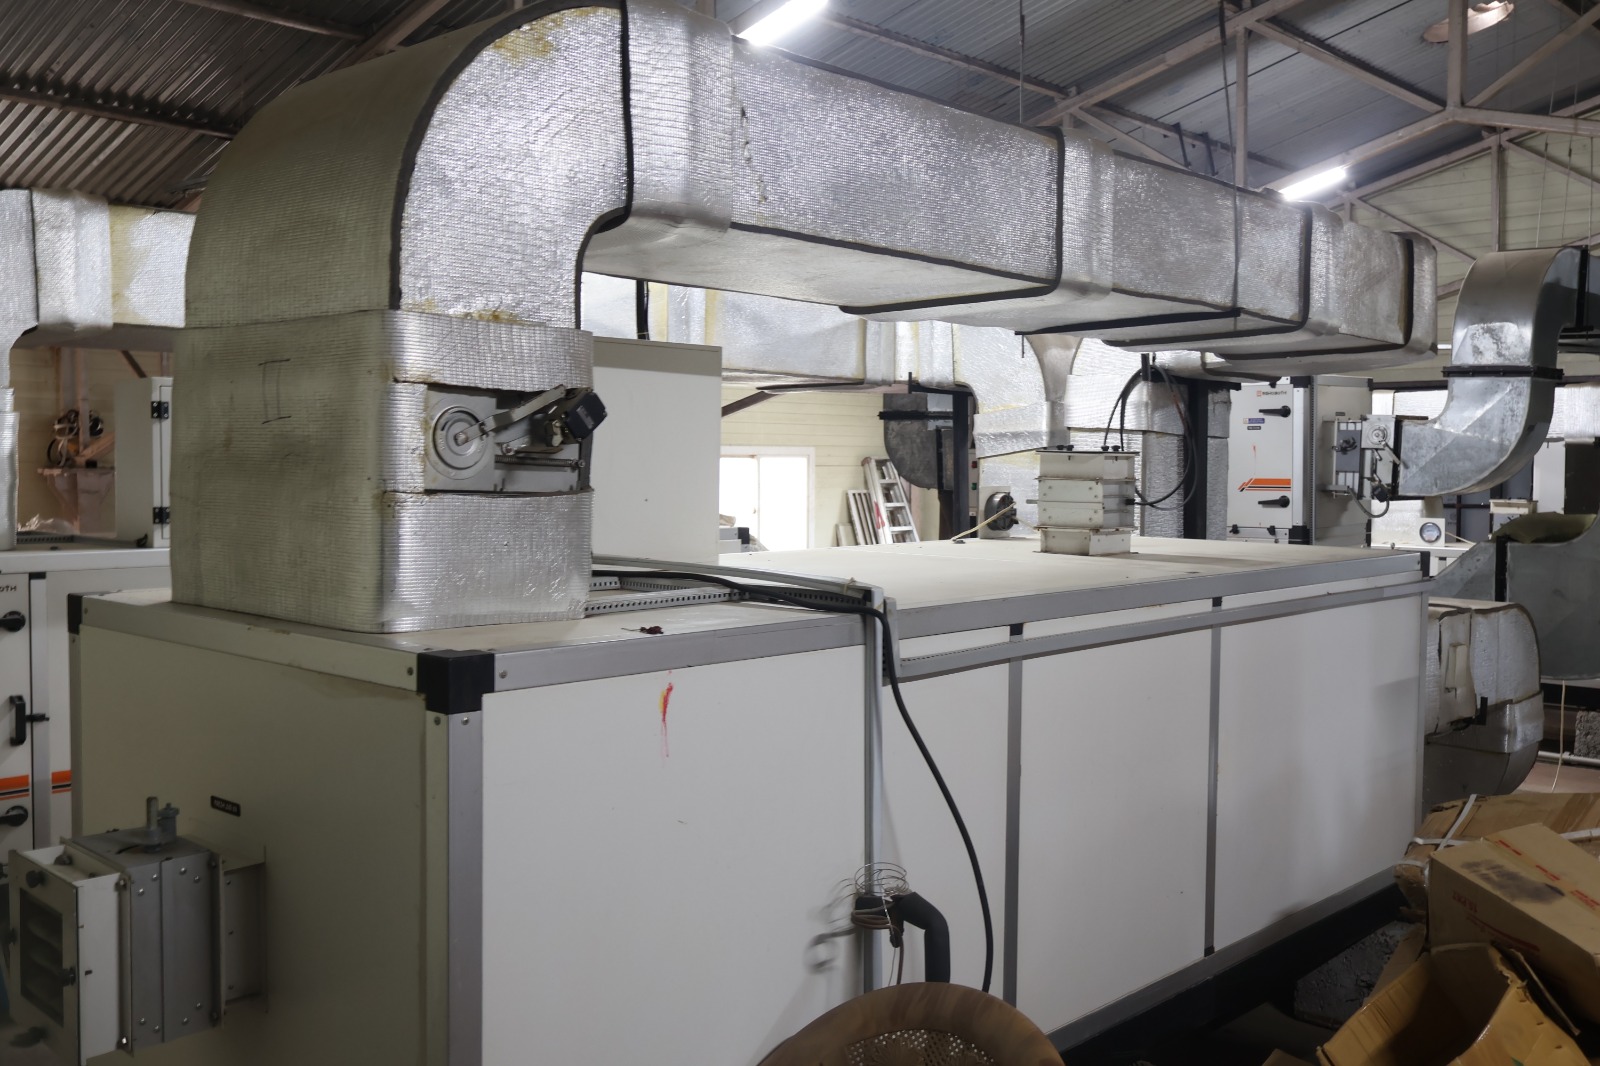
99.97% particulate arrestance at 0.3-micron threshold, driving continuous negative-pressure air volume changes and 45–55% relative humidity control.
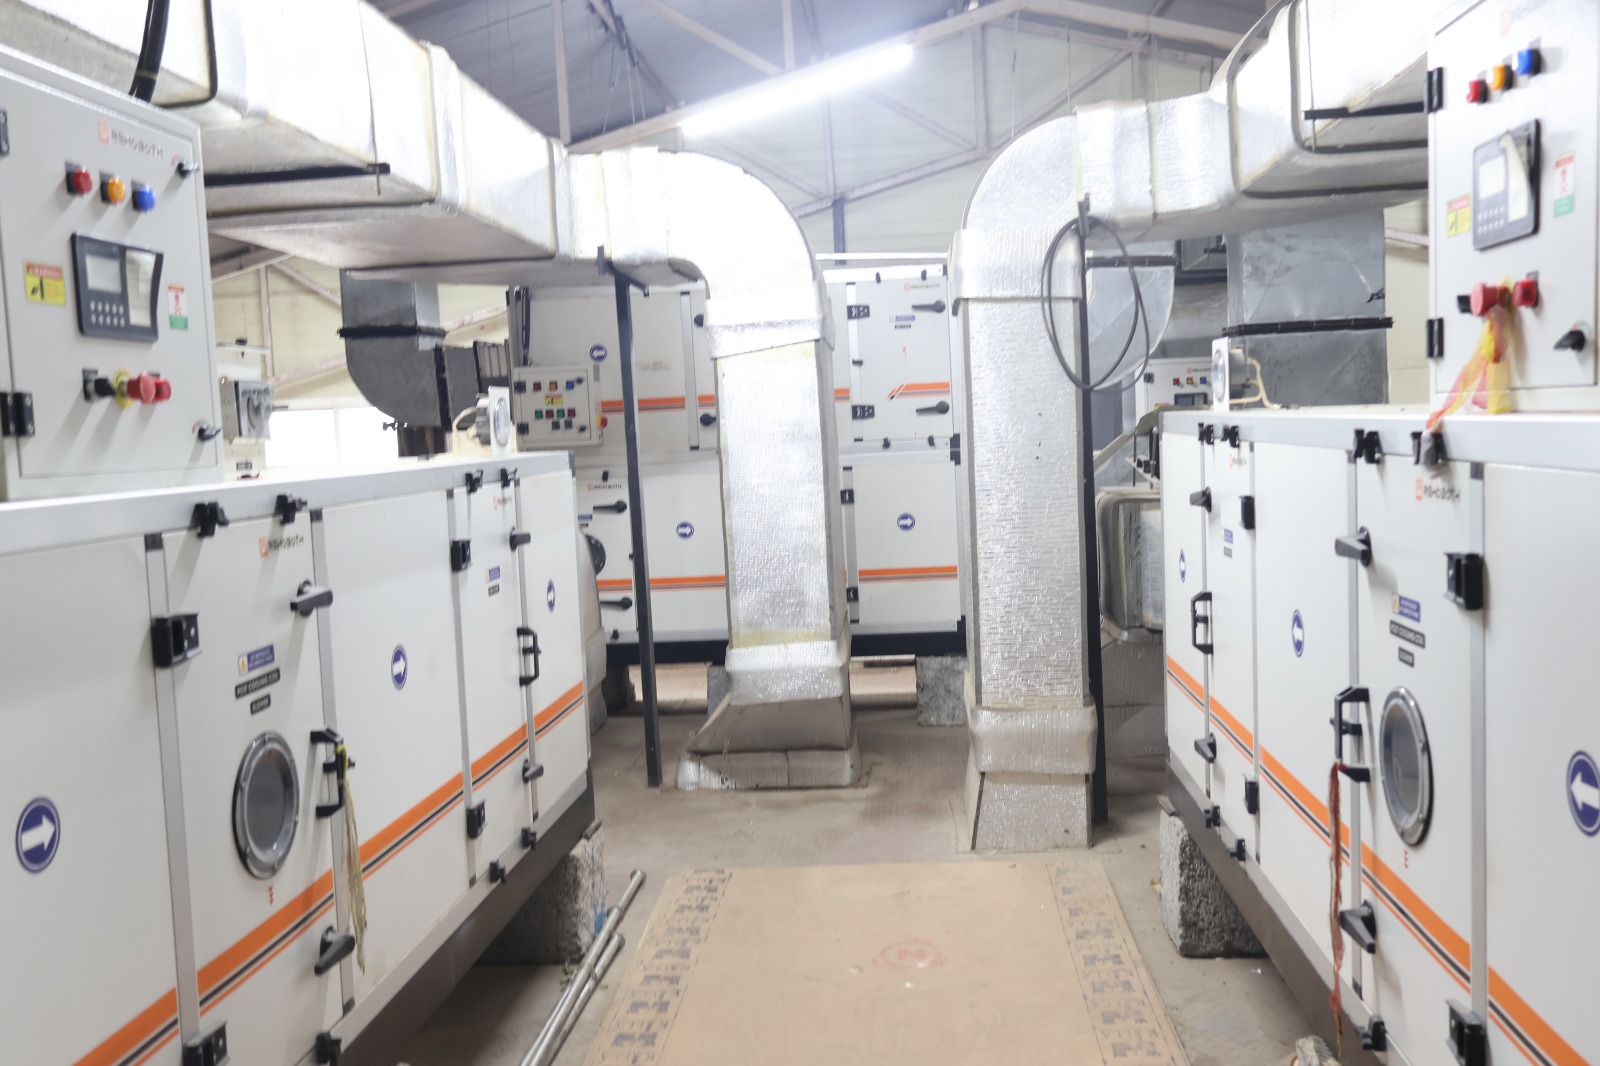
99.97% particulate arrestance at 0.3-micron threshold, delivering continuous laminar air volume changes across compounding suites and filling corridors.
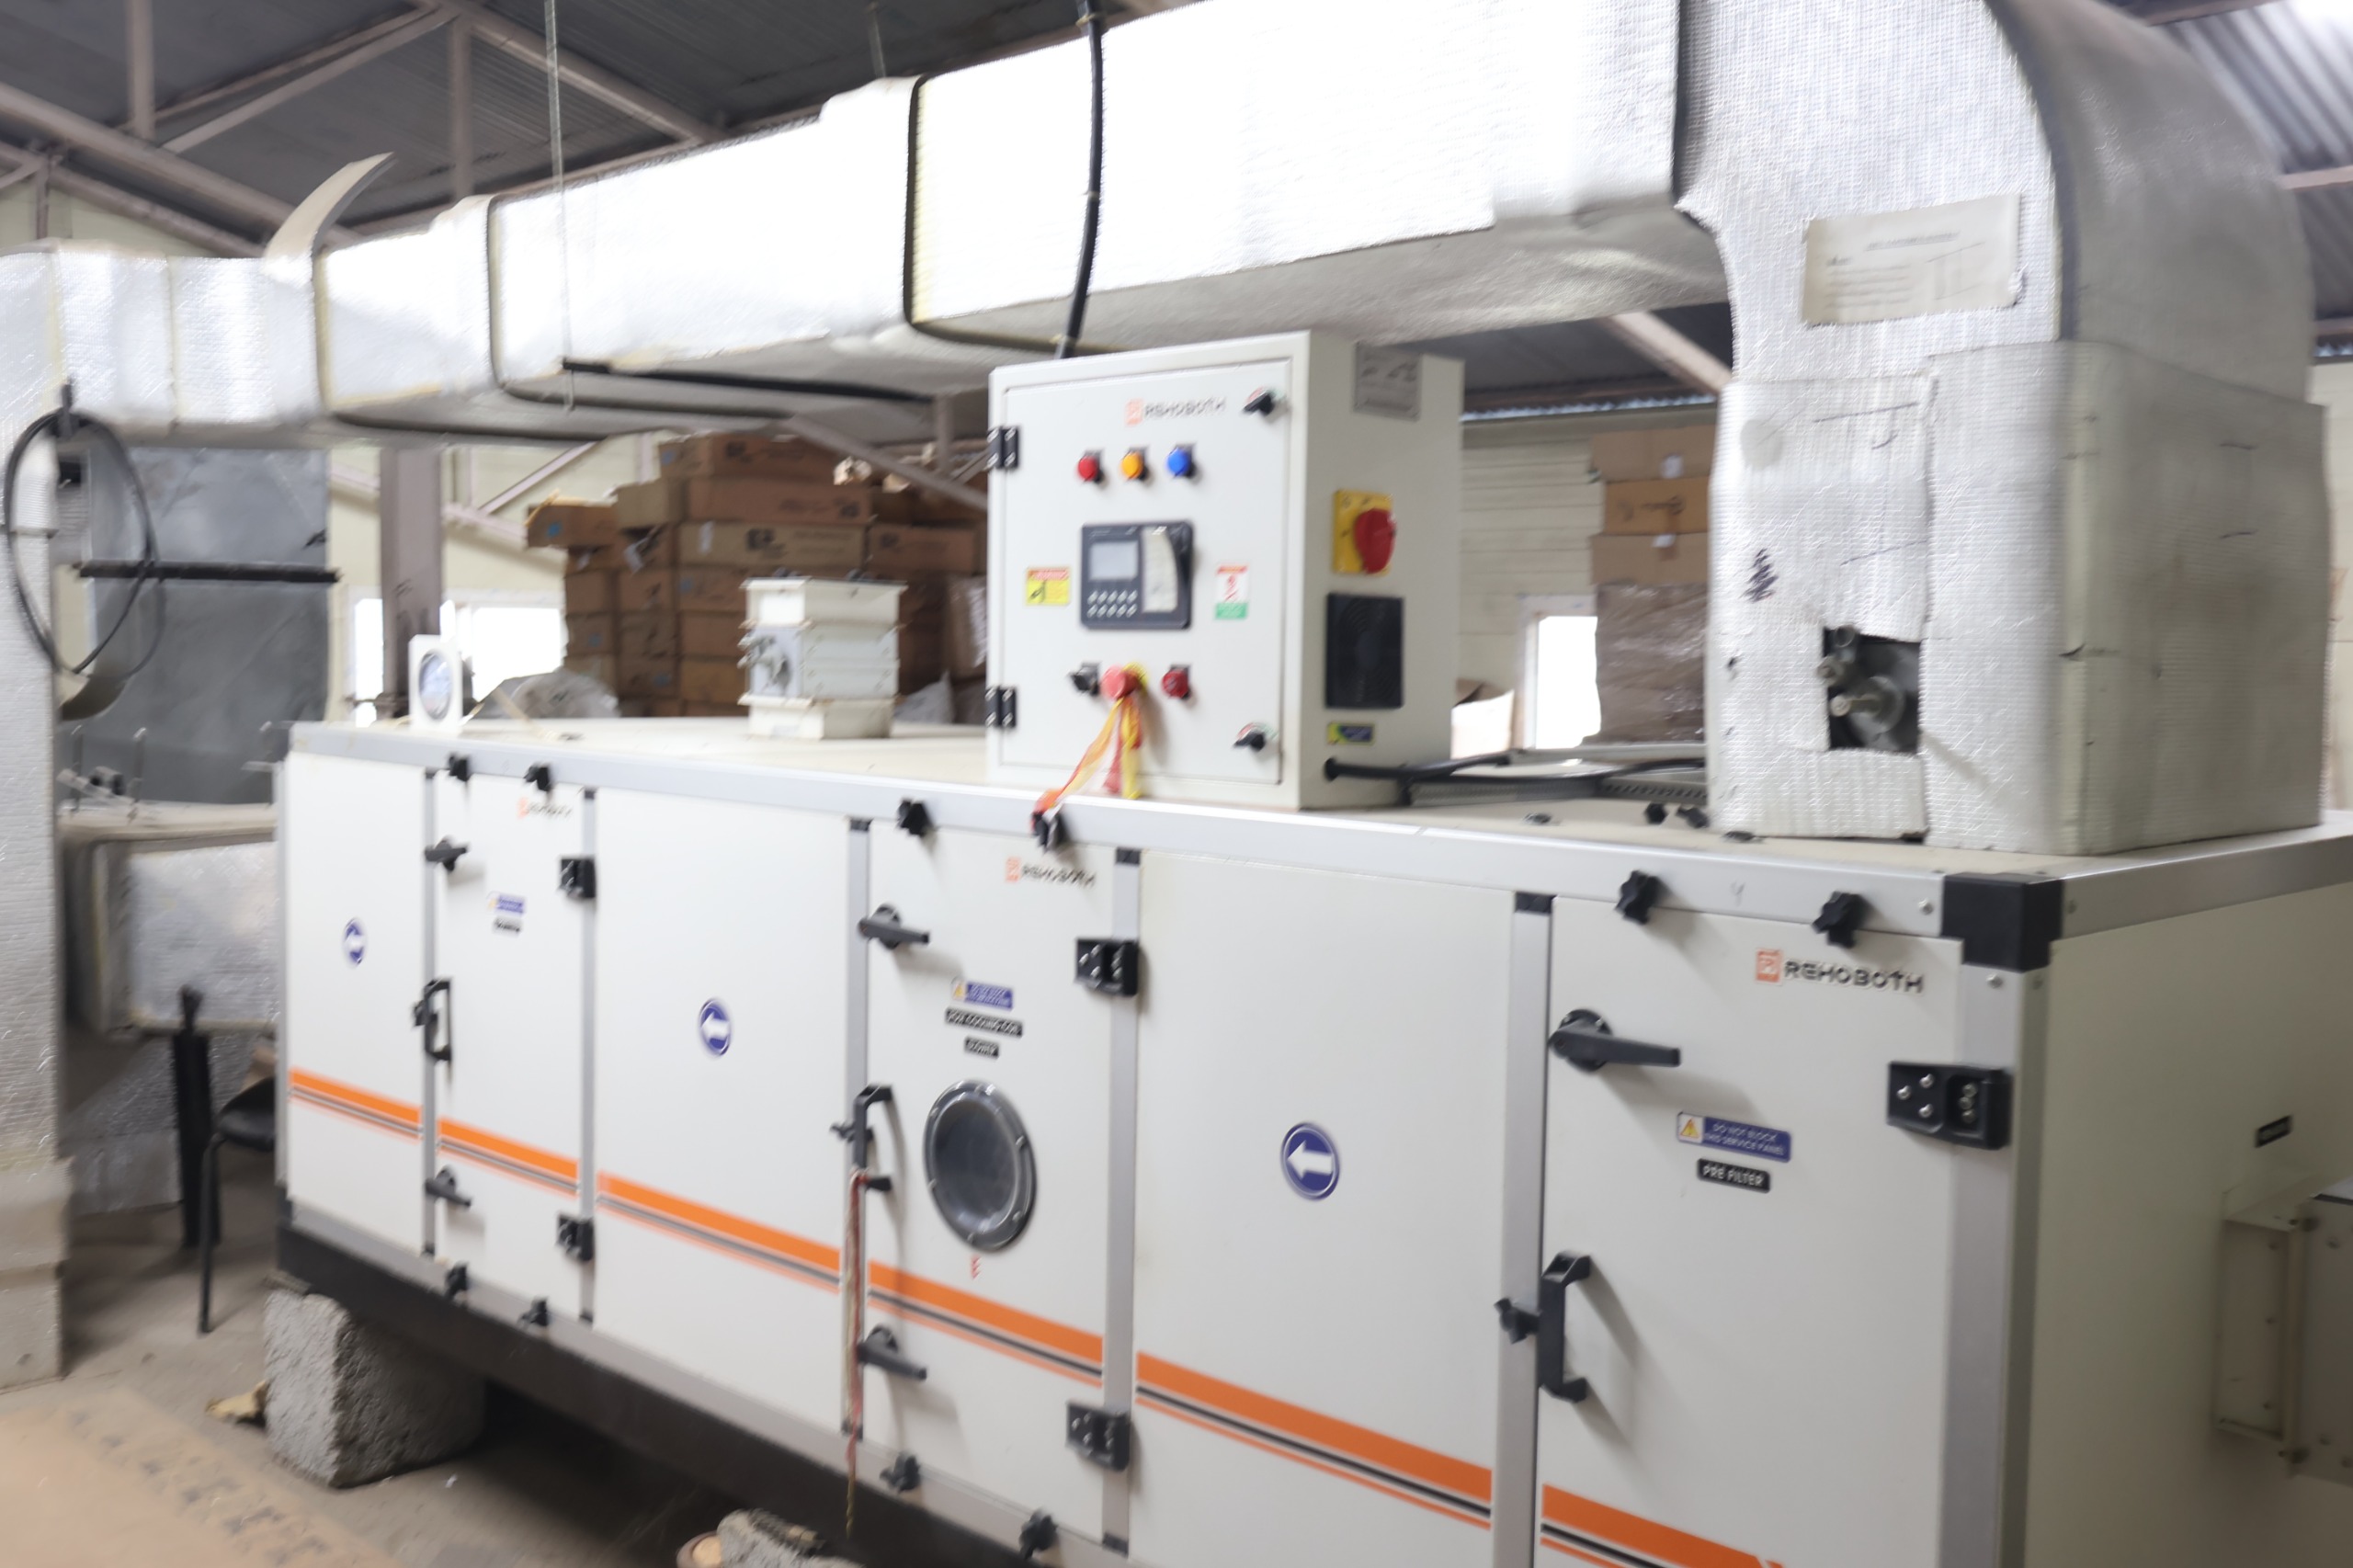
99.97% particulate arrestance at 0.3-micron threshold, maintaining dedicated independent environmental zoning and sterile airflow for analytical laboratories.
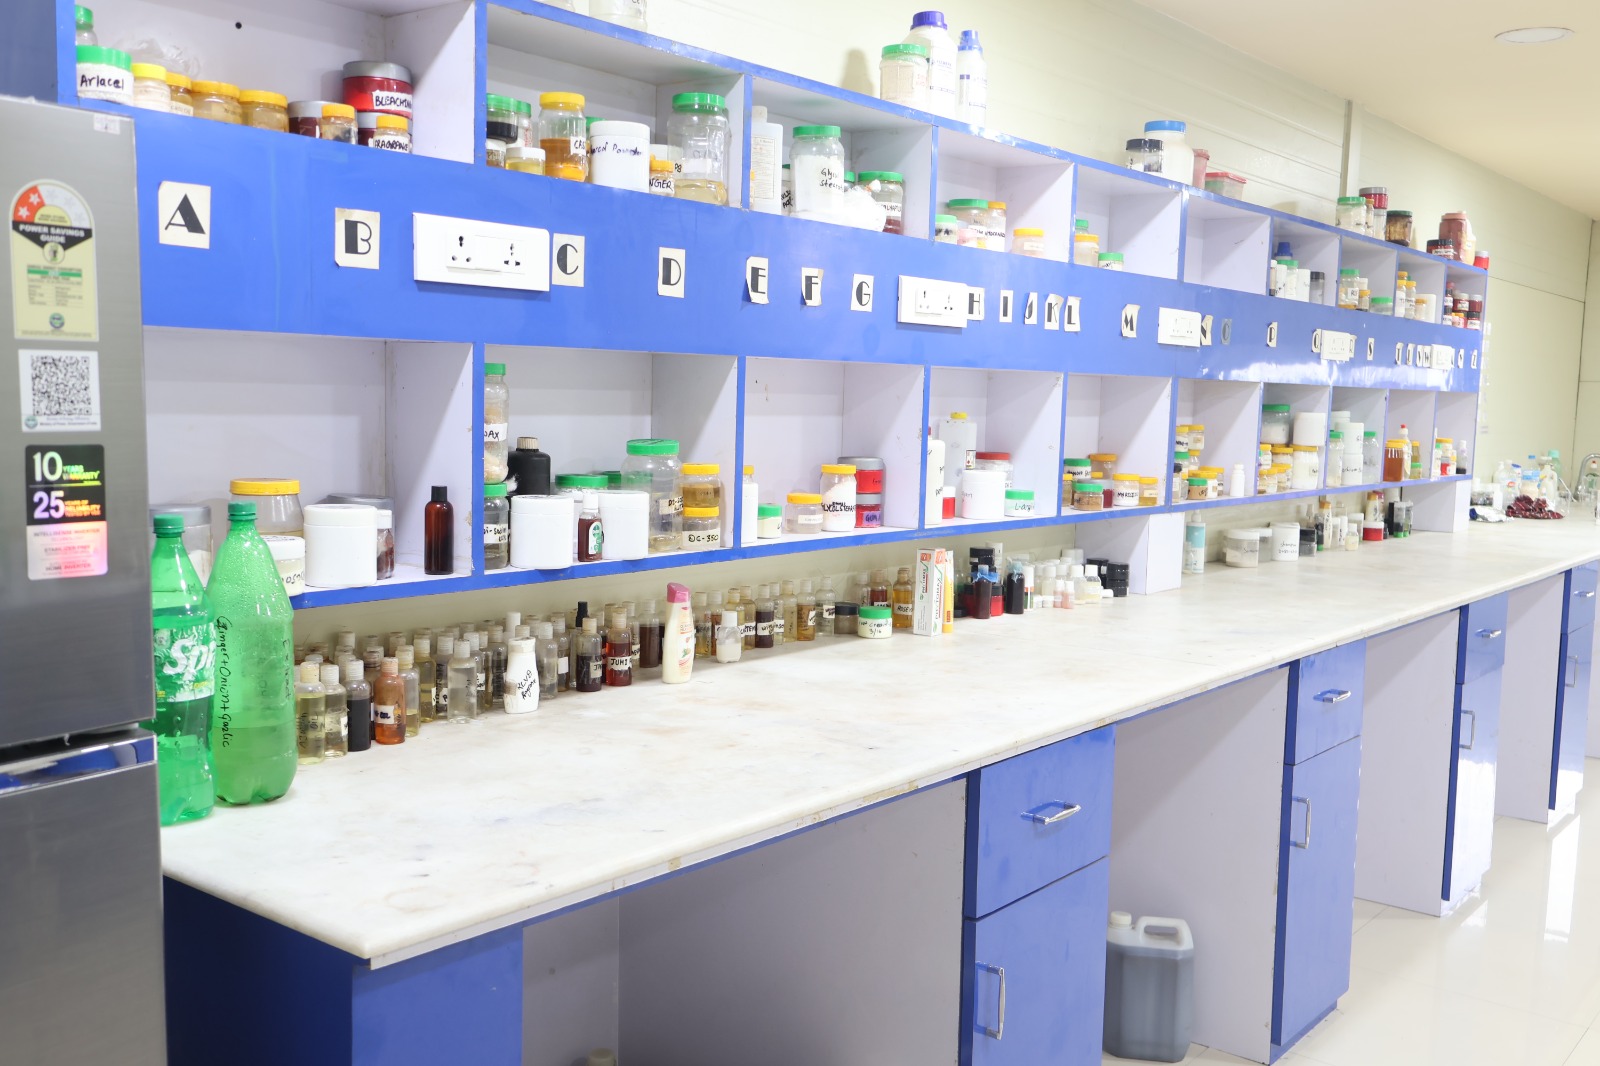
Physical property benchmarking, emulsion shear stability, and thermal accelerated ovens.
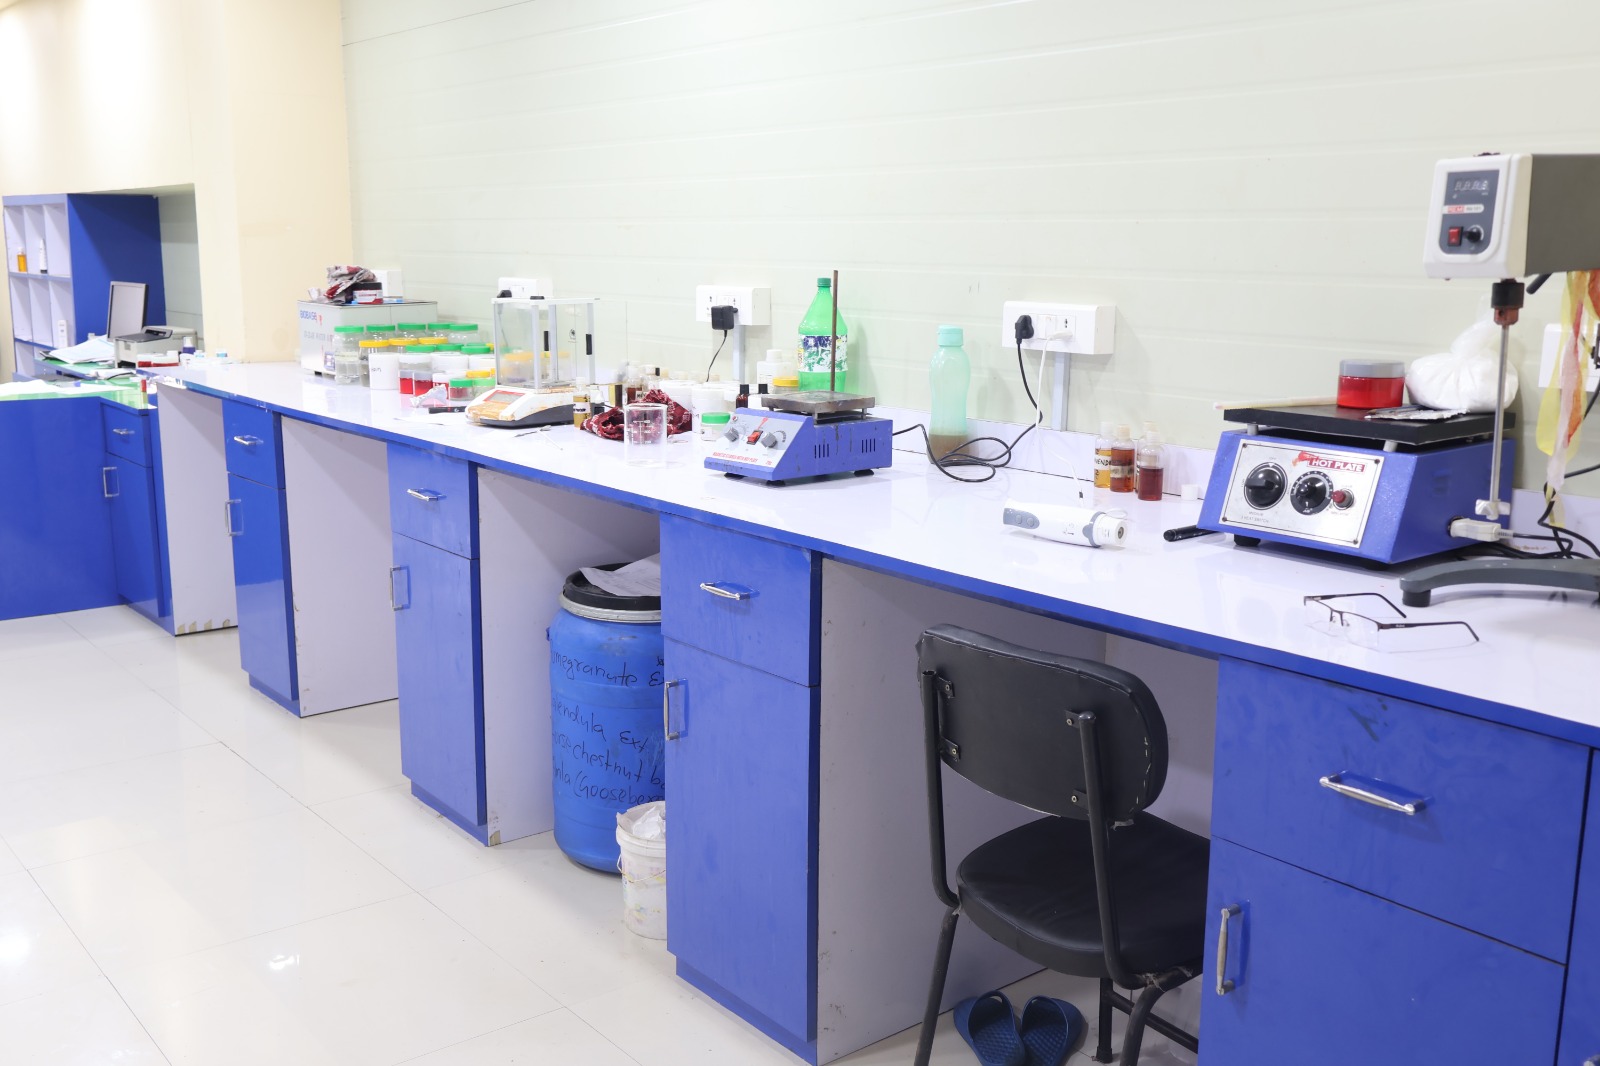
Sterility assurance testing verifying formulations remain free from pathogen contamination.
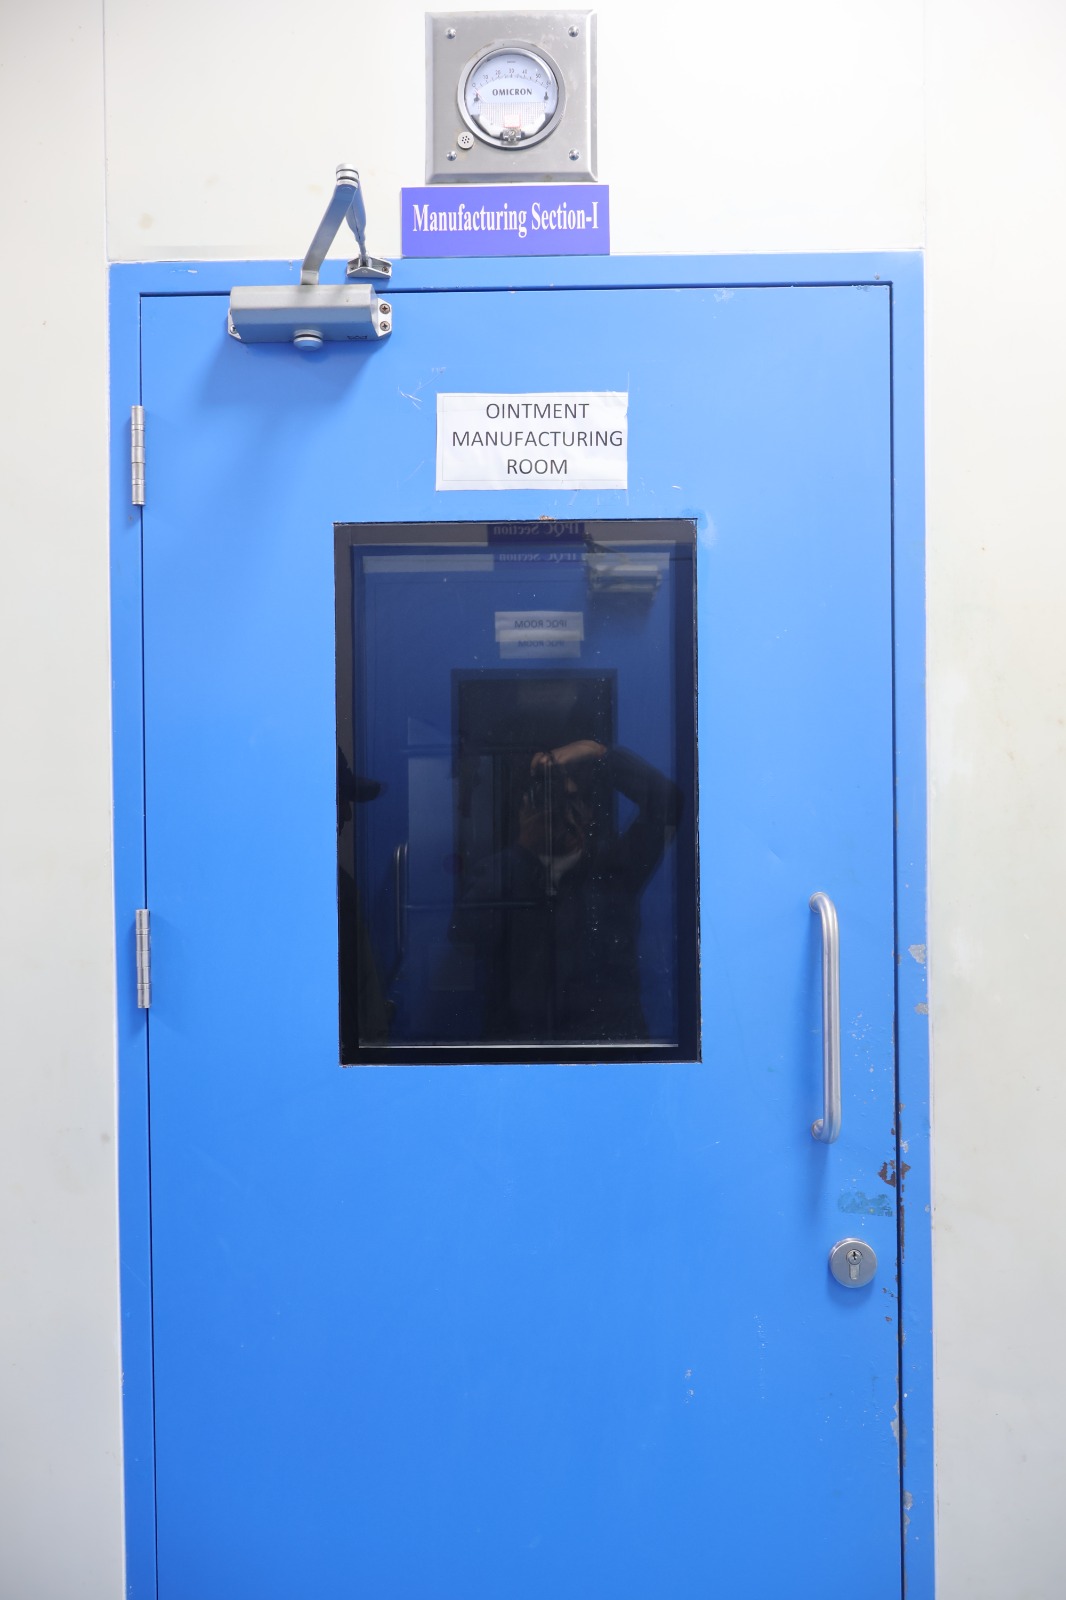
High-shear sanitary homogenizers preventing atmospheric particle deposition during batch blending.
Anti-static sealed corridors with negative-pressure differential cascade airlocks between gowning and production zones.
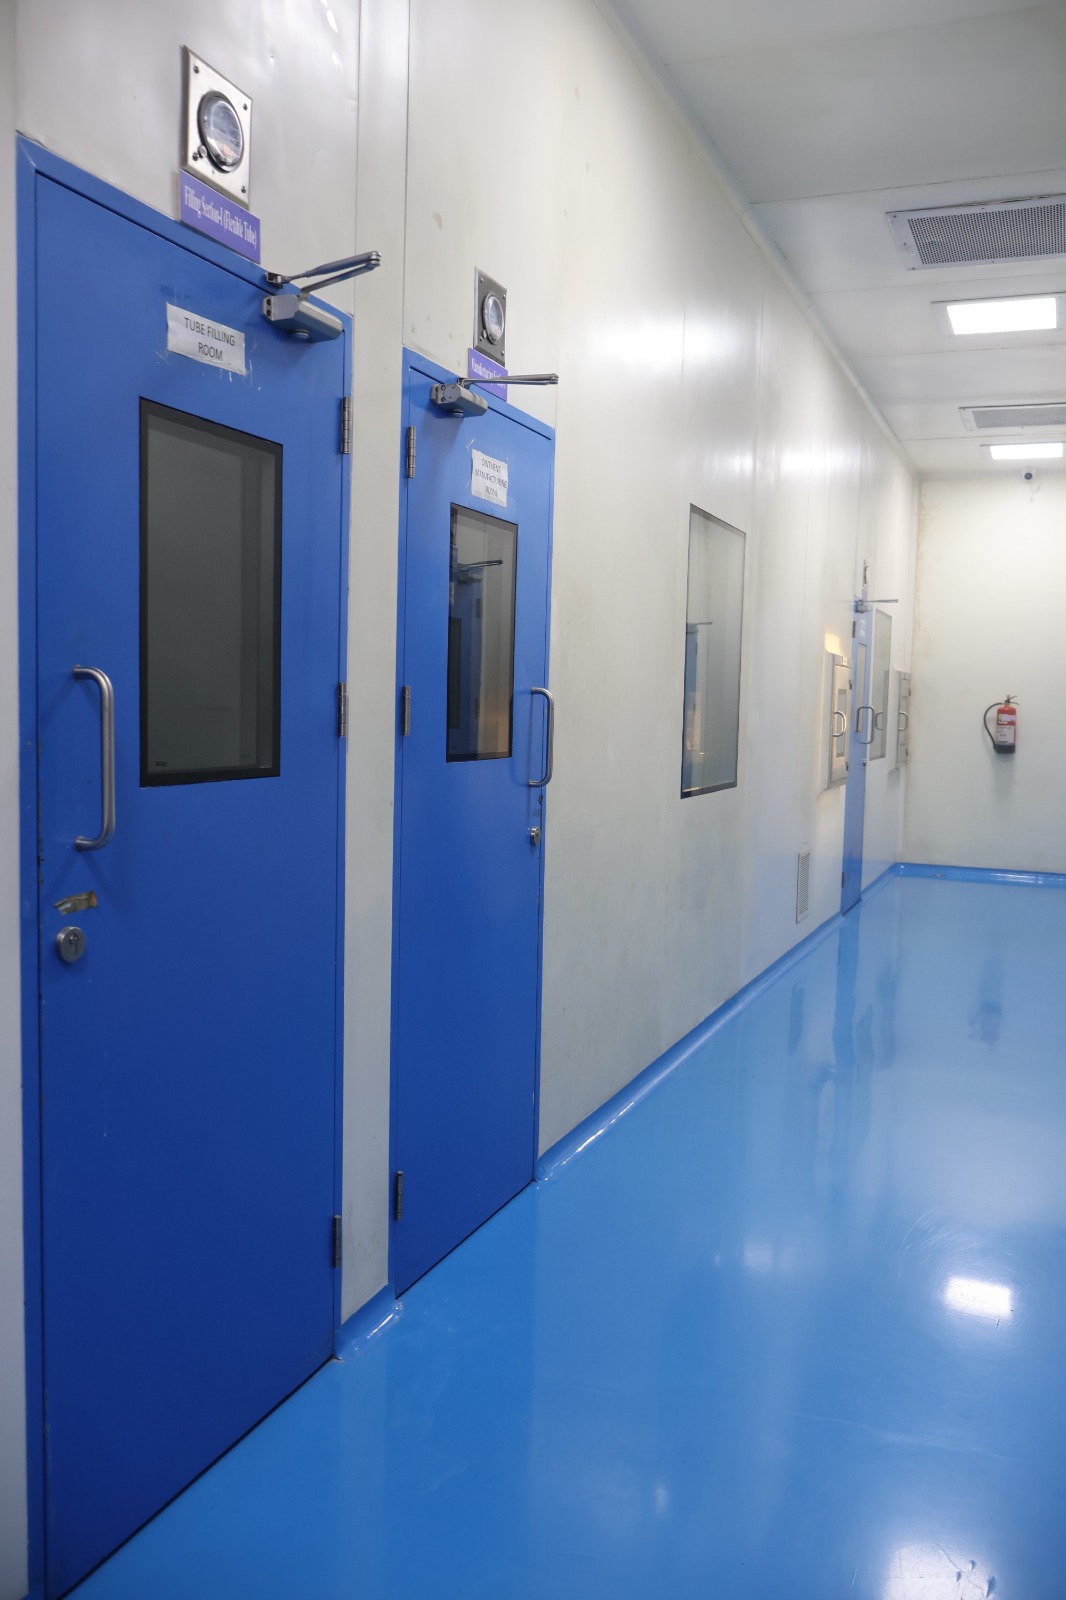
Secondary atmospheric barrier and cleanroom gowning transitional hall isolating sterile processing from logistics.
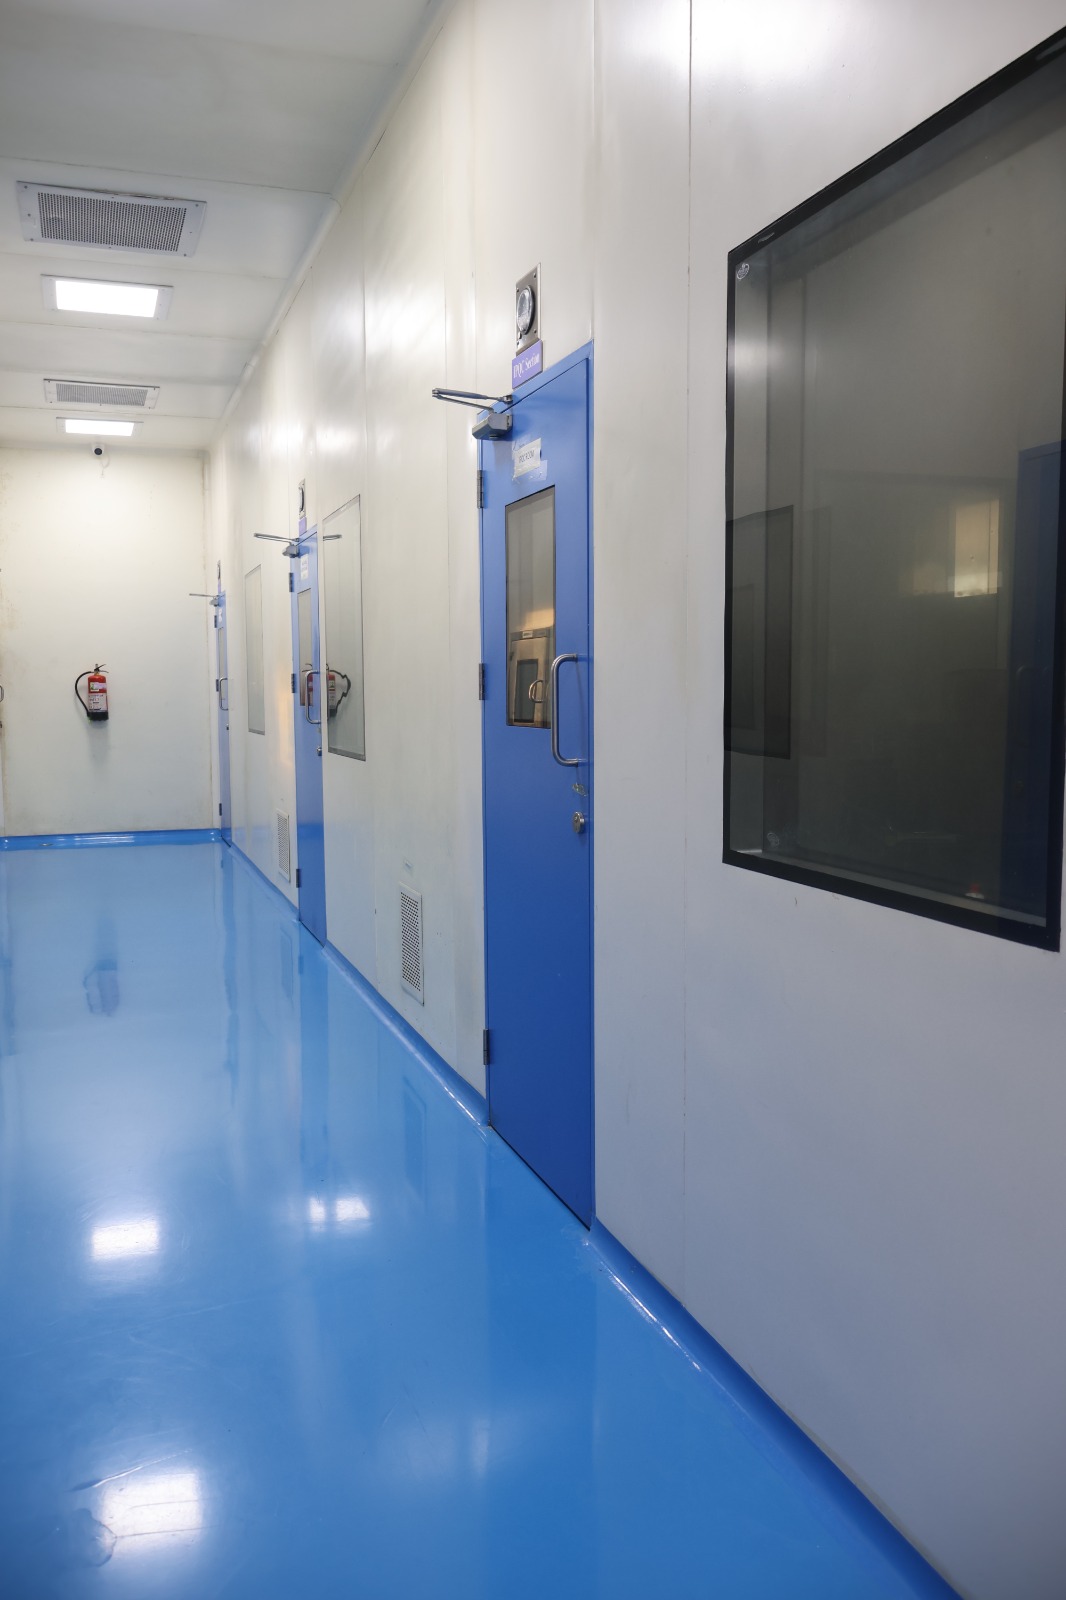
Seamless pharmaceutical-grade epoxy floors and coved baseboards allowing continuous sterile washdown cycles.
Phytomax Care Pvt. Ltd. publishes only factual, verifiable quality and testing information. Any specific laboratory certifications or clinical testing accreditations are verified internally prior to public claim verification.
Our Mandatory Release Protocols:
Authorized Personnel can request official technical documentation, Certificates of Analysis (CoA), or verification samples directly from our corporate office in Bharatpur-16, Chitwan.
Phytomax Care Pvt. Ltd. — Direct Verification & Communication Desk